
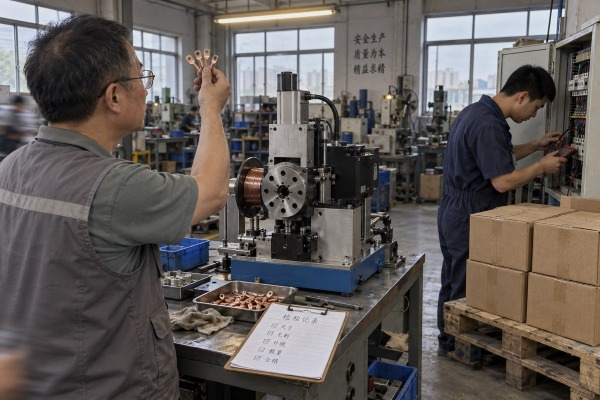
A cable lug making machine can pass a showroom demo and still fail on your floor. At our Wenzhou factory, we see this risk often—third-party inspection prevents it.
Arrange third-party inspection by booking an ISO 17020-accredited agency for a Factory Acceptance Test 5–7 days before shipment, after full commissioning. Check crimp quality, output speed, hydraulic pressure, electrical safety, tooling, documentation, and packaging, then tie final payment to a passed report.
That is the short answer. The longer answer covers timing, agency selection, the exact test items, and what to do when the report finds problems. Let me walk through each step.
A procurement manager in the US once asked us to inspect his cable lug machine before commissioning. We told him to wait—and here is why timing matters.
The best time is 5–7 days before shipment, after the machine is fully assembled, commissioned, and able to run continuous production. For custom or large orders, add a during-production check midway through the build and a formal Factory Acceptance Test.

Timing is the part most buyers get wrong. If the inspector arrives too early, the machine cannot run real production. The inspector will see a frame, some wiring, and a promise. If the inspector arrives too late, the machine is already crated. Nobody can open the electrical cabinet or run a trial batch. The 5–7 day window before shipment solves both problems. The machine is finished and stable. There is still time to fix defects before the vessel booking closes.
For a standard machine, one pre-shipment inspection 1 is often enough. For a custom crimping line or a high-volume order, we recommend a staged plan. In our own export projects, we send the client our internal quality control checklist 2 and test protocol before assembly even starts, so the acceptance criteria are locked in writing from day one.
| Stage | When | Purpose |
|---|---|---|
| Document review | Before assembly begins | Agree on acceptance criteria; review the supplier's own inspection list and machine validation documents |
| During-production check | Mid-build (custom or large orders) | Verify frame quality, hydraulic components, and brand parts before panels enclose them |
| Main pre-shipment inspection / FAT | 5–7 days before shipment, after full commissioning | Witness continuous production runs against written criteria |
| Reinspection | After corrective actions | Confirm all defects are closed before final payment |
Some buyers ask whether they can skip this entirely and rely on the supplier's internal QC to save a few hundred dollars. I understand the instinct, but the math rarely works. A single bad machine means delayed production, rework costs, and freight for return shipments. The inspection fee is small compared with that risk. Tie your final payment to the inspection result in the contract, and the schedule enforces itself.
We weigh one trade-off with every export order: a big-name agency's credibility versus a machinery specialist's technical depth. Both matter when verifying a cable lug making machine.
Choose an independent agency with ISO 17020-style accreditation and proven industrial machinery experience—SGS, TÜV, or Bureau Veritas are common choices. Avoid consumer-goods generalists. Give the inspector a detailed Technical Requirement Document before assembly is finalized so they test against measurable criteria.

The agency's name matters less than two qualities: independence and machinery competence. ISO 17020-style independence means the inspector has no commercial tie to the supplier. Machinery competence means the inspector has actually tested hydraulic presses, PLC control system logic 3, and terminal feeding lines before—not just counted cartons of consumer goods. An inspector who has never watched a vibratory bowl feeder jam will not know what to look for.
Travel cost and lead time push many buyers toward remote verification, and it has become genuinely workable. Here is how the two options compare:
| Factor | On-site inspection | Remote (online) FAT |
|---|---|---|
| Confidence level | Highest; inspector touches the machine | High, if multi-camera video and recorded evidence are used |
| Cost and speed | Travel fees, scheduling delays | Cheaper, can be booked within days |
| Dispute resolution | Easier; physical measurements on record | Depends on quality of recorded proof |
| Best for | Custom lines, first orders, large contracts | Repeat orders, standard machines, urgent shipments |
In our own practice, we run the remote option as a formal online acceptance meeting. Before the meeting, we send the client our full inspection checklist and every test item. During the meeting, our engineers demonstrate each point live on camera and record the details one by one. Afterward, we hand over all the videos and photos so the client keeps permanent evidence. Whether you hire SGS or accept a structured remote FAT, insist on this level of documented proof. Vague verbal assurance is worth nothing six months later.
During one online acceptance meeting, our engineers ran the vibratory feeder and crimping station live for two hours while the client's inspector logged every reading. That session shaped this checklist.
Ask the inspector to verify crimp quality and dimensional accuracy against DIN, UL, or IEC lug standards, production cycle time at full capacity, hydraulic press performance, die hardness (HRC), electrical safety and CE compliance, brand-name component authenticity, documentation, and packaging readiness.

A good inspection is a structured test, not a walk-around. Give the inspector measurable pass/fail criteria for each category. Here is the core quality control checklist we recommend, grouped the way a professional FAT report is usually organized:
| Category | What the inspector should verify |
|---|---|
| Machine function | Start-up, stop, emergency stop response, alarm handling, interlocks, light curtains |
| Output performance | Production cycle time at full capacity over sustained multi-run trials; speed matches the contract |
| Crimp quality | Crimp height, shape, compression integrity, and repeatability across sample lugs |
| Dimensional accuracy verification | Lug dimensions and tolerances against DIN, UL, or IEC standards; die alignment |
| Tooling and die specifications | Correct die set, no wear or cracks, HRC hardness test on crimping dies and cutting molds, ease of changeover |
| Hydraulic and pneumatic systems | No leaks, pressure stability, force accuracy, smooth actuation; origin of pumps and valves |
| Electrical safety | Cabinet build, wiring, grounding, guarding, CE certification compliance or UL where required |
| Documentation | Electrical schematics, PLC logic diagrams, maintenance manuals, wear parts list, calibration records, material test report for key components |
| Packaging | Corrosion protection, secured moving parts, labeling, complete accessories |
First, thermal imaging during the trial run. A thermal camera reveals abnormal heat in motors, bearings, or the electrical cabinet—early signs of misalignment or poor wiring. Second, component authenticity. If the contract promises a Siemens PLC or Schneider electrics, cross-reference the serial numbers with the manufacturer. Counterfeit industrial parts do circulate. Third, software access. Confirm you receive administrative passwords and parameter access so you can troubleshoot without depending on the supplier forever. We flag these three points to clients before every acceptance meeting because they cause the most disputes after delivery.
Early in our export business, we learned that an unaddressed minor defect becomes a major dispute after shipment. Handling inspection findings properly protects both buyer and supplier.
Classify findings as critical, major, or minor. Require corrective action for all critical and major defects, demand a documented fix with photo or video proof, book a reinspection, and hold final payment until the closure report confirms every non-conformity is resolved.

A defect finding is not a disaster. It is exactly what you paid the inspector to find. What matters is the process you follow next. A professional report already gives you the structure: sample size, defect severity, pass/fail result, photos, and corrective action requirements. Your job is to act on it methodically.
| Severity | Typical example | Required action |
|---|---|---|
| Critical | Emergency stop fails; crimp force out of spec; safety guard missing | Must be fixed and reverified; shipment blocked |
| Major | Hydraulic leak; wrong die set; missing PLC logic diagrams | Must be fixed before shipment; documented proof required |
| Minor | Surface scratch; label misprint; loose cable tie | Fix before packing or accept with written note |
One lesson we pass to every client: raise the contentious points with your supplier in advance, before the inspection ever happens. Crimp tolerance ranges, acceptable cosmetic marks, and speed measurement methods are the classic argument triggers. When we handle acceptance for our own machines, we discuss these sensitive items with the buyer beforehand and write the agreed interpretation into the test protocol. Then the reinspection becomes a simple verification, not a negotiation. Never let the supplier pressure you into releasing final payment "on good faith" while critical or major items remain open—payment control is your only real leverage once the machine leaves the factory.
A bad machine costs months; an inspection costs days. Define criteria early, choose a machinery-experienced inspector, verify everything on video, and never release final payment before closure.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
1. Standard industry practice for verifying equipment quality and specifications before international shipping. ↩︎
2. ISO 9001 provides the framework for quality control checklists and management systems in manufacturing. ↩︎
3. Technical overview of the programmable logic controllers used to automate industrial machinery. ↩︎
