
A cable lug making machine can look perfect in a demo. On our Wenzhou production line, I have watched “perfect” samples hide burrs, weak crimps, and drifting tolerances.
To design a test checklist for a cable lug making machine, list every test item and acceptance standard in advance, provide product drawings to the supplier, verify dimensions, pull-out force, conductivity, and plating against a named standard like IEC 61238-1, and record yield and scrap rates across a sustained run.
That single paragraph is the whole strategy. But each item hides real detail. Below, I break the checklist into four parts: performance parameters, dimensional checks, supplier QC standards, and durability testing. Follow them in order, and a misleading sample will never get past you.
A procurement manager from Ohio once asked me over WhatsApp: “Jane, which numbers actually matter?” We built his parameter sheet together in one afternoon, and it changed his sourcing results.
Include cycle speed, hydraulic system pressure stability, crimp force repeatability, pull-out force measurement, electrical resistance or millivolt drop, plating thickness, and forming completeness. Test each parameter against a named standard such as IEC 61238-1 or UL 486A-486B, not against visual impressions alone.

The biggest mistake I see is mixing up two different jobs. You must verify the machine, and you must verify the product. They are related, but they are not the same thing.
Machine verification covers alignment, tooling stability 1, repeatability, and safety. Product verification covers the lug itself: geometry, surface condition, and performance after the cold forging process. A machine can pass one check and fail the other. That is why your test checklist needs both columns.
Here is the core parameter table I share with buyers before any sample run:
| Parameter | How to Test | Acceptance Basis |
|---|---|---|
| Cycle speed | Timed production run | Supplier’s rated output claim |
| Hydraulic system pressure | Gauge reading during run | Stable, no drift under load |
| Crimp quality | Crimp cross-section analysis | Terminal crimping specifications, no voids |
| Pull-out force measurement | Tensile strength test 2 on crimped samples | IEC 61238-1 or UL 486A-486B limits |
| Electrical resistance | Millivolt-drop test vs. equivalent conductor | Electrical conductivity standards |
| Forming completeness | Visual and gauge check | No incomplete forming or flash |
Two tests deserve special attention. First, the pull-out test. A crimp must hold under rated tension, and only a tensile strength test proves it. Second, resistance profiling. A properly formed lug should perform close to the conductor’s own resistance. In our experience, micro-structural grain flow analysis 3 via cross-sectioning is also worth requesting on high-value orders. It reveals internal stress fractures or material thinning in the transition zone that no surface inspection can catch. Treat pull-force and resistance checks as mandatory release gates, not optional extras. That is exactly how leading procurement teams now structure their approvals.
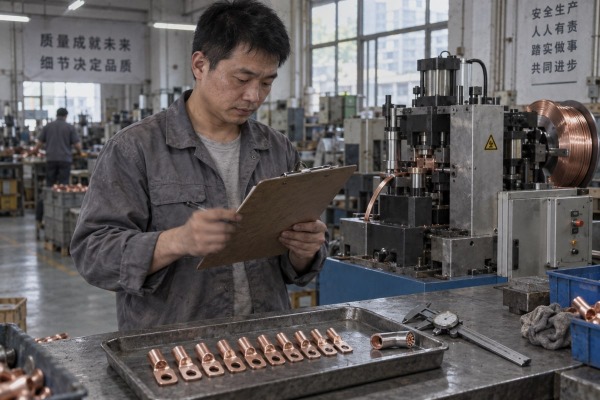
During one acceptance run at our Wenzhou workshop, a caliper caught a slow barrel-diameter drift around piece 300. No human eye would ever have noticed it in time.
Verify dimensional accuracy by measuring barrel internal diameter, stud hole diameter, wall thickness, tube diameter, palm thickness, and overall length with calipers or gauges. Then confirm consistency by sampling across a 500-piece run and calculating the Process Capability Index (Cpk) to detect drift.

Dimensional checks fail buyers in one predictable way: they measure one piece. One good piece proves nothing. Inspection specs use random sampling from lots for a reason, and sample size should grow with lot size. Never accept a single “golden sample.”
Your drawing should define every critical dimension before the supplier starts. This is the exact practice I follow with my own customers: we set the acceptance criteria and receive the product drawings 4 before we cut a single piece of copper. Here is my standard dimensional sheet:
| Dimension | Tool | Immediate Rejection Trigger |
|---|---|---|
| Barrel internal diameter | Plug gauge or caliper | Out of drawing tolerance |
| Stud hole diameter | Pin gauge | Inconsistent hole size across samples |
| Wall thickness | Micrometer | Thinning in the transition zone |
| Tube diameter | Caliper | Ovality beyond tolerance |
| Palm thickness | Micrometer | Deviation from DIN 46235 or UL 486A-B dimensions |
| Overall length | Caliper | Cumulative drift over the run |
Consistency lives in the numbers, not the sample tray. Ask the supplier to run at least 500 pieces, pull samples at set intervals, and calculate Cpk. This exposes drift in automated production before you pay for it. Two more checks reveal machine health indirectly. First, measure the “flash” or excess material at the seam. Heavy flash signals poor hydraulic stability or tool misalignment. Second, confirm the die set tolerance in writing, because worn or loose dies are the root cause of most dimensional drift. Finally, check marking legibility: wire size, stud hole diameter, and branding should be clearly embossed and centered on the palm on every sampled piece, not just the first one.
Early in our export business, I assumed a certificate PDF meant compliant parts. One difficult shipment to a German customer taught me that paper and product are two very different things.
Request one governing standard (IEC 61238-1, DIN 46235, or UL 486A-486B), written pass/fail acceptance criteria, material purity verification via spectrometer, plating thickness reports, dimensional inspection sheets, pull-out test records, and a video-recorded live production run before approving any sample.

The rule I now apply on every project is simple: define the checklist and the acceptance standard before production, not after. In my own buying and selling practice, I list every test item in advance, set written acceptance criteria, hand the supplier the product drawings, and require yield and scrap data from the sample run. “Looks good” is not a standard.
Your market decides your standard. Do not let the supplier pick for you:
| Standard | Primary Market | What It Governs |
|---|---|---|
| IEC 61238-1 | International / EU projects | Compression connector electrical and mechanical performance |
| DIN 46235 | Germany and DIN-based markets | Cable lug dimensions and tolerances |
| UL 486A-486B | United States and Canada | Connector safety, pull-out, and temperature performance |
If you sell into the US, UL 486A-486B compliance shapes your entire checklist. If you sell into Germany, DIN 46235 defines your dimensional sheet. When we prepare Factory Acceptance Test documents for our US and German buyers, the standard is named on page one.
Beyond the standard, request a full documentation set: spectrometer results confirming ETP copper grade for material purity verification, tin-plating thickness and uniformity measurements, salt spray resistance results for corrosion performance, dimensional reports on measured samples, pull-out test records, production parameter logs, a spare parts list, and photos of tooling and packaging. Record sample IDs and machine settings so every sample traces back to its exact configuration. Some buyers argue certification alone is enough. I disagree from experience: certificates prove a system exists, but only sample-based verification proves this machine, with this tooling, makes conforming parts. Third-party inspection or a video-recorded live run closes that gap.
Every buyer weighs the same trade-off: pay less and test after delivery, or invest two extra days in a supervised endurance run. Our engineers always advise the second path.
Test durability by running the cable lug making machine continuously for several hours or 500+ pieces under a Factory Acceptance Test protocol. Record yield rate, scrap rate, hydraulic pressure stability, and temperature drift, and approve only if quality holds across the entire run.

Some buyers prioritize price and capacity, arguing that testing can wait until the machine arrives. I understand the schedule pressure. But the risk is real: you may pay for a fast machine that cannot hold tolerances under continuous load. Shipping it back across an ocean costs far more than a two-day acceptance run. Here is the endurance procedure we run at our factory before any balance payment.
Only release the balance payment after the documented run passes. When we ship equipment to the United States, Japan, or Germany, this exact sequence is what protects both sides of the deal.
A beautiful sample can hide an unreliable machine. Define your checklist first, name your standard, demand documented tests, and release payment only after a successful live production run.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
