
Buyers often ask our Wenzhou team where the final payment milestone should sit when buying an automatic assembly machine. Many got burned by “balance on shipment” terms and lost leverage.
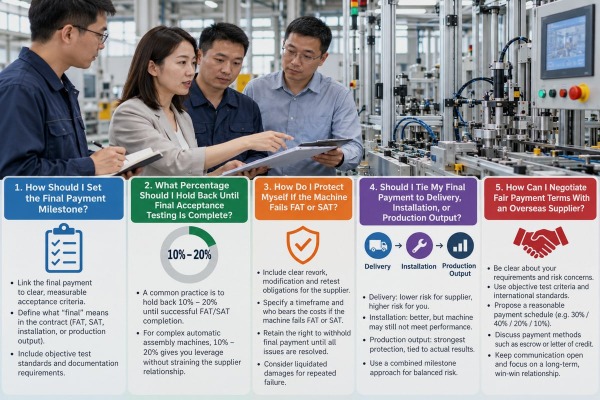
Set the final payment milestone at documented site acceptance, not shipment. Pay 10–15% after a successful Site Acceptance Test in your plant with your materials, and retain 5–10% until the automatic assembly machine completes an agreed period of stable production.
That is the short answer. The rest of this article explains how to size the holdback, how to protect yourself when a test fails, which trigger to choose, and how to make the terms fair for an overseas supplier. I write this from the supplier side, because we build these machines and we sign these contracts every month.
A German buyer once offered to pay 90% before our cable lug assembly line even left Wenzhou. I asked him to keep more back.
Hold back 15–25% of the price until final acceptance testing is complete. Release 10–15% after a signed Site Acceptance Test, and keep a further 5–10% as retention payment for 30–90 days of stable production or punch list completion.

Why did I ask that buyer to hold more? Because a buyer who has already paid almost everything has no reason to work with us on ramp-up issues. He just gets angry. A buyer who still holds 15% stays engaged, sends us data, and signs the final acceptance certificate when the machine proves itself. That is healthier for both sides.
The table below shows a structure we see often. It is an example, not a rule.
| Milestone | Typical share | What the buyer should see before paying |
|---|---|---|
| Contract signing | 20–30% | Signed contract, FAT and SAT protocols attached |
| Design approval | 10–20% | Approved layout, tooling drawings, controls documentation |
| Mechanical completion or pre-FAT review | 20–30% | Photos, build records, inspection evidence |
| Successful Factory Acceptance Test 1 | 20–30% | Signed FAT protocol, recorded run, open-issues list |
| Delivery, installation, and successful Site Acceptance Test 2 | 10–20% | Signed SAT, training records, documentation package |
| Stable production or defect-liability period | 5–10% | Agreed run period completed, punch list closed |
Published machinery contracts 3 vary. One custom-machine guide uses 20–30% at signing, 15–20% after design approval, 20–25% after mechanical completion, 20–25% after FAT, and 10–15% after SAT. Another industrial example retains 10% for 30–90 days after continuous production use. Some turnkey schedules reserve a final 5% until the defect-liability period ends.
The right number follows risk. I ask three questions. How customized is the machine? How hard is it to replace? How integrated is it with other equipment? A standard chamfering machine 4 with a two-week lead time needs a smaller retention. A multi-station assembly line with two bowl feeders, vision inspection 5, and an MES link needs a larger one. The more a machine can only be judged on your floor, the more value should stay unpaid until it performs there.
Suppliers will push back. Retention ties up cash and may raise the quoted price. That objection is fair. My answer is to keep the retention small, define its end date clearly, and never let it drift. A 5–10% retention with a fixed 30–90 day clock costs us little. An undefined "balance after everything is fine" costs us a lot, and we will price for it.
Every acceptance clause we write balances two risks: a buyer rejecting a good machine over small issues, and a supplier calling real failures "commissioning issues."
Protect yourself by attaching written FAT and SAT protocols to the contract, with measurable pass/fail thresholds, a defined supplier cure period, retesting rights, and payment withheld in proportion to the failure. Classify defects as major or minor so safety and cycle time failures block acceptance.

The best protection is written before the machine is built. A Factory Acceptance Test protocol drafted after mechanical completion will reflect what the machine can do, not what you ordered. So we ask buyers to approve the test protocol at design approval. It lists each test step, the measurement method, the equipment used, and the pass/fail threshold.
A failure is not a crisis if the contract already says what happens next. Our clauses usually follow this sequence:
Not every defect should stop payment. A missing label should not hold 15% of a contract. A machine that damages terminals should. The table below shows how we split the two.
| Category | Examples | Effect on payment |
|---|---|---|
| Major defect | Cycle time below contract, yield below threshold, safety guarding fault, component damage, failed integration with feeders or conveyors | Blocks acceptance and the related milestone until corrected and retested |
| Minor defect | Cosmetic paint marks, missing label, incomplete non-critical manual section, loose cable tray | Goes on the punch list; payment released minus a small holdback until punch list completion |
| Documentation gap | Missing PLC backup, as-built electrical schematics, spare parts list | Treated as major if critical for maintenance; otherwise punch list |
The Factory Acceptance Test happens in our environment, so you should demand hard evidence. Ask for a signed protocol, a recorded production run, serial numbers of tested tooling, actual cycle-time and quality data, alarm logs, a safety-function checklist, and confirmation that the shipped configuration matches the tested one. Remote FAT by live video works well for overseas buyers who cannot travel. Add an independent inspector if the project is large.
One more point. For a turnkey line, avoid all-or-nothing payment. Pay for stations that have standalone value, but keep enough retention to cover whole-line performance. One incomplete station can idle the whole line.
A procurement manager in Mexico asked me last year: "Why not just pay when the machine arrives?" My answer was blunt: arrival proves nothing about output.
Tie the final payment to production output verified during a Site Acceptance Test, not to delivery or installation alone. Delivery proves shipment, installation proves the machine powers up, but only output with your materials, operators, and interfaces proves the automatic assembly machine does its job.

Here is how the common triggers compare.
| Payment trigger | What it actually proves | Risk left with the buyer |
|---|---|---|
| Shipment notice | The supplier dispatched a crate | Transit damage, wrong utilities, failed integration, low output |
| Factory Acceptance Test | The machine ran in the supplier's shop | Site conditions, real materials, operator skill, plant interfaces |
| Installation and commissioning | The machine is powered, programmed, and cycles | Sustained output, reject rates, jam frequency, software faults |
| Site Acceptance Test | The machine met contract performance in your plant | Problems that appear only over several shifts |
| Stable production period | The machine held performance after our technicians left | Very little |
Our own advice to every buyer is simple. Link the balance to the Factory Acceptance Test, to installation and commissioning on your site, and to final acceptance. Never let a shipment notice alone release the final payment. A notice from our logistics desk tells you a container left Ningbo. It does not tell you that your bowl feeder will orient your parts at speed, or that your compressed air is dry enough, or that your conveyor handshake works.
Buyers often confuse commissioning with acceptance. Commissioning means our engineer energized the machine, loaded the program, debugged the stations, and ran operator training. That is real work. But it does not prove machine cycle time over a full shift. A machine can pass a short Site Acceptance Test and still fail during ramp-up because of feeder instability, sensor drift, overheating, or operator-dependent performance.
Write the test around commercial operation, not around "it cycles." Useful criteria include:
Some buyers go further. They add a 90-day OEE stability window after our technicians leave, a cybersecurity review of remote access before network integration, or an energy audit comparing actual power and compressed-air consumption with the quote. We accept these when the thresholds are measurable and written in advance. The two-stage model handles this well: release one portion after formal SAT, and hold the remainder until the stability window closes.
Exporting to the US, Germany, and Japan taught our small team one lesson: payment terms feel fair only when both sides can see what triggers each release.
Negotiate fair terms by trading a reasonable deposit for a meaningful retention payment, defining buyer site-readiness duties, using objective acceptance criteria, and adding security tools such as a letter of credit, performance bond, or neutral inspector. Set deadlines and deemed-acceptance rules so neither side waits indefinitely.

Fair does not mean soft. It means each side carries the risk it can control. We control design, build quality, and performance guarantees. You control site utilities, sample supply, operator availability, and the acceptance decision. A good contract names both lists.
| Supplier concern | Buyer concern | Balanced clause |
|---|---|---|
| Excessive retention raises financing cost | Paying 90% before production leaves no leverage | Cap retention at 5–10% with a fixed 30–90 day clock |
| Failures often come from poor utilities or untrained operators | Suppliers relabel real faults as "commissioning issues" | Define site-readiness duties; log root cause in the protocol |
| Acceptance should not depend on a plant manager's mood | A machine that runs but misses output has not delivered its purpose | Use measurable thresholds for cycle time, yield, and uptime |
| Buyer delays should not block payment forever | Deemed acceptance can hide safety defects | Allow deemed acceptance only after proper notice, never for safety or major performance failures |
| Indefinite liability for production losses is unfair | Enforcement against an overseas supplier is slow | Limit remedies to defined amounts; appoint a neutral engineer for disputes |
Distance adds risk for both of us. A machine can reach your dock while our technician waits for a visa. These tools help, and each should be discussed with commercial counsel:
Before agreeing to the final payment milestone, confirm that SAT criteria are in the contract, tests use production-intent materials, cycle time and quality thresholds are measurable, run duration is specified, integration with adjacent equipment is included, safety compliance is a condition of acceptance, operator training and documentation are deliverables, punch list treatment is defined, failed-test remedies and retesting are written, a retention payment survives ramp-up, the person who signs the final acceptance certificate is named, buyer-caused delays are separated from supplier-caused failures, and payment timing, currency, taxes, and inspection evidence are unambiguous.
In my experience, buyers who bring this checklist to the first call get better prices. Clear terms lower our risk, and lower risk lowers the quote.
Paying on shipment leaves you powerless. Split the final payment milestone: release part after a documented SAT, hold the rest until stable production. Verified performance, not delivery, earns payment.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
1. Provides a technical overview of the Factory Acceptance Test process used to verify equipment before shipment. ↩︎
2. The International Trade Administration provides guidance on international procurement standards and technical requirements for exporters. ↩︎
3. The ITC offers model contracts for the international sale of goods, including machinery and equipment. ↩︎
4. ISO standards provide safety and quality requirements for industrial machine tools and automated equipment. ↩︎
5. IEEE develops technical standards for the sensors and vision systems used in automated industrial inspection. ↩︎
