
Last month, a U.S. buyer asked our Wenzhou team to defend a fully automatic pipe cutting machine test report line by line. One vague standard reference nearly killed the deal.
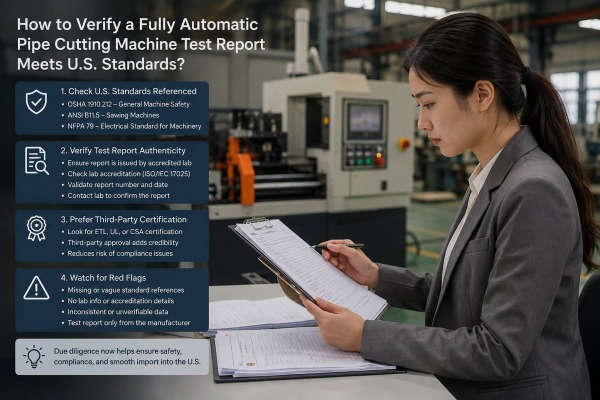
To verify a fully automatic pipe cutting machine test report meets U.S. standards, check five things: the exact standards cited (OSHA, ANSI B11, NFPA 79), the test items covered, data authenticity, third-party or NRTL recognition, and safety compliance evidence like guarding and emergency-stop tests.
Those five checks come straight from how I audit our own paperwork before export. In this article, I will walk through each one. You will learn which standards apply, how to spot fake data, when third-party certification matters, and which red flags should stop a purchase cold.
Two machines left our floor last quarter with two different standards packets. Same brand, same buyer, different cutting methods. That single detail changed which ANSI B11 standards applied to each report.
Your test report should reference OSHA 1910 Subpart O machine guarding, the applicable ANSI B11 machine-safety standard for your cutting method, NFPA 79 for electrical design, OSHA 1910.95 for noise, and an ANSI/ISO 12100 risk assessment covering automated cycles.

Here is the first thing I tell every procurement manager: there is no single "U.S. standard" for pipe cutters. U.S. compliance is a stack. OSHA safety compliance sits at the top as the legal layer. ANSI B11 standards form the consensus layer that shows how you satisfy OSHA. NFPA 79 covers the electrical panel. Some buyers assume only OSHA matters. That view is incomplete. OSHA's guarding rule is broad. It says the point of operation 1 must be guarded so no body part can enter the danger zone during the cycle. ANSI B11 tells you how to achieve that for a specific machine type.
Another common mistake is assuming all pipe cutters use the same standard. They do not. A cold saw, an abrasive cutter, and a thermal cutter fall into different categories. The ANSI B11 family includes 26 standards plus several technical reports. If the machine also bends or shapes tube, ANSI B11.15 applies. If it uses flame cutting, OSHA's welding and cutting rules enter the picture too. Classification comes first. Compliance verification comes second.
| Standard | What It Covers | Why the Report Needs It |
|---|---|---|
| OSHA 1910 Subpart O | Machine guarding, point of operation | Legal requirement for U.S. workplaces |
| ANSI B11 series | Machine-specific safety design | Shows how OSHA expectations are met |
| NFPA 79 | Industrial machinery electrical design | Disconnects, grounding, control circuits |
| OSHA 1910.95 | Noise exposure limits | Operators work near the machine daily |
| ANSI/ISO 12100 | Risk assessment methodology | Documents residual risks in automatic cycles |
| ASTM metal standards | Material and cut integrity | Validates results on the actual alloy processed |
Our engineers also cross-reference cut precision against relevant ASTM metal standards for the specific alloy. A report that names the exact sub-standard, not just "ANSI," is the report you want.
There is a real trade-off I weigh on every export order: verifying paperwork adds days before shipment, but skipping it invites returns and after-sales disputes. I always choose the extra days.
Confirm authenticity by matching the report's serial number and model to the actual machine, checking instrument calibration records, verifying signatures and test dates, requesting raw data and video evidence, and validating results yourself during a Factory Acceptance Test before shipment.

A fabricated report usually fails on details, not headlines. When I review quality assurance documentation 2 from any source, I start with identification. The report must name the machine serial number, model, revision, test date, test location, test method, and acceptance criteria. Then I check who signed it and whether that person is qualified. Vague sign-offs are a warning. ASTM E4, which governs force verification of testing machines, is a useful benchmark here. It is not about pipe cutters. But it shows what rigorous verification looks like: clear machine ID, verified ranges, dates, agency name, and error-free documentation. Hold your supplier's report to that structure.
Every measurement in the report came from an instrument. Ask for the equipment calibration records behind each one. If the caliper or laser gauge used for dimensional tolerance verification has no valid calibration certificate, the numbers are unverifiable. On our line, we keep calibration files linked to each test sheet for exactly this reason.
Material traceability matters more than most buyers expect. Cut accuracy on soft demo stock proves little. Ask whether the test pipe came with a Mill Test Report MTR. Then ask the supplier to repeat key cuts on your actual pipe material during a live Factory Acceptance Test 3 FAT. We run FATs over video call for U.S. clients who cannot fly to Wenzhou. Watching the emergency stop get pressed in real time beats any PDF.
| Authenticity Check | What to Request | Failure Signal |
|---|---|---|
| Machine identity | Serial number, model, revision on report | Generic report with no serial number |
| Measurement validity | Equipment calibration records | Expired or missing certificates |
| Material relevance | Mill Test Report MTR for test stock | Unknown or ideal-only demo material |
| Live proof | Witnessed or filmed FAT | Supplier refuses video verification |
| Data depth | Raw data sheets, not just summaries | Suspiciously uniform, rounded numbers |
A procurement manager in Ohio once messaged me on WhatsApp with one question: "Is your panel UL listed?" His plant inspector would not energize any machine without NRTL backing. That question deserved a precise answer, not a sales pitch.
Yes, for the electrical system insist on NRTL certification (UL, Intertek ETL, or CSA), because U.S. inspectors and insurers recognize it. For mechanical performance, a manufacturer's report is acceptable if you witness a Factory Acceptance Test and receive full supporting documentation.

Some suppliers will tell you their own certificate is enough. I disagree, and I say that as someone who issues certificates. A self-declaration that does not name the exact standards, test methods, and machine configuration proves very little. Buyers increasingly want test evidence, not just declarations. At the same time, demanding third-party certification for everything is neither practical nor necessary. The smart approach splits the report into layers.
| Evidence Layer | Manufacturer Report OK? | Third Party Needed? |
|---|---|---|
| Cut accuracy and repeatability | Yes, with witnessed FAT | Optional |
| Squareness and burr quality | Yes, with raw data | Optional |
| Electrical panel safety | Supporting only | Yes, NRTL (UL/ETL/CSA) |
| Software and control reliability | Supporting only | Recommended (UL 1998) |
| Noise levels vs OSHA 1910.95 | Yes, with calibrated meter data | Optional |
Our position is simple. We provide our own FAT records, technical data sheet, and schematics, and we support NRTL evaluation on the electrical side when the buyer's site requires it. The extra cost is small compared to a machine an inspector refuses to approve.
Early in our exporting years, I learned a hard lesson: a competitor's machine reached a U.S. client with a glowing report, then failed a plant safety audit in one afternoon. The report had measured everything except safety.
Major red flags include vague phrases like built to ANSI standards, missing calibration data, no risk assessment, no emergency-stop or interlock test records, performance data without safety evidence, and a declaration that does not name your machine's serial number or exact standards applied.

The most dangerous belief in this market is "if it cuts accurately, it must be compliant." Precision and throughput prove nothing about guarding, control safety 4, or maintenance access. A machine can hold tight tolerances and still let an operator reach into the blade zone. So when I audit a fully automatic pipe cutting machine test report, I read it like an inspector, not like a salesperson. The document should prove the machine is safe, identifiable, and testable under the correct U.S. standards. Not merely that it cut pipe well once.
| Red Flag | What It Hides | What to Demand Instead |
|---|---|---|
| "Built to ANSI standards" with no number | Nobody matched the machine to a real standard | Exact ANSI B11 sub-standard citation |
| No emergency-stop or stop-time data | Untested safety circuit | Recorded stop-response test results |
| No mention of safety interlock systems | Guards may open during the cycle | Interlock function test on each movable guard |
| No lockout/tagout provisions listed | Maintenance staff face live energy | Documented energy isolation points |
| No risk assessment attached | Residual risks were never analyzed | ANSI/ISO 12100 risk assessment |
| No noise measurement | Possible OSHA 1910.95 exposure issue | Calibrated sound level data |
| No coolant or lubricant disclosure | Chemical compliance gaps | Proposition 65 or TSCA documentation |
| Catalog specs instead of machine data | Report describes a different unit | Serial-matched report and technical data sheet |
First, check for human factors. ANSI/HFES 100 guidance on interface and control layout reduces operator fatigue and error, and strong reports address it. Second, check that the report matches the machine as installed, not the catalog version. Configuration changes between quotation and delivery are common, and paperwork rarely keeps up unless someone forces it to.
Weak paperwork causes expensive surprises after installation. Audit the standard basis, test items, data authenticity, third-party recognition, and safety compliance before you pay. A verifiable report protects your production line.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
1. Official OSHA resource defining machine guarding requirements and point of operation safety standards. ↩︎
2. Official ISO page for quality management standards governing quality assurance documentation and verification. ↩︎
3. Authoritative engineering reference explaining the purpose and procedure of a Factory Acceptance Test (FAT). ↩︎
4. OSHA standard 1910.212 covering general safety requirements and control safety for industrial machinery. ↩︎
