
Our Wenzhou workshop ships cable lug machines to ten countries, and I have watched a vague quality objection period clause breed months of disputes latent-defect rights 1. A segmented clause fixes that.
Specify a segmented quality objection period in your cable lug machine contract: 48 hours for transport damage, 7–14 days for visible defects, acceptance-based deadlines for performance issues, and discovery-based notice for latent defects. Require written notice with photo evidence, parts-first remedies, and cap total compensation at the machine price.
That is the short version. The rest of this article shows how to write each part. I will cover the objection clause itself, the claim procedure, the time frames worth negotiating, and the steps that protect your rights when the machine misses its specifications. I write from the seller’s chair, but I will be honest about where buyers should push back.
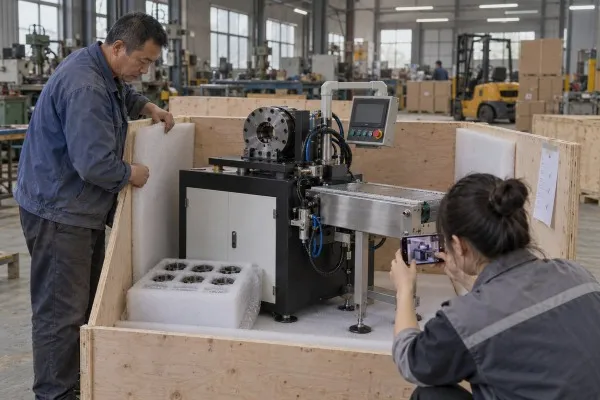
Last year a crate reached Slovakia with a dented control cabinet door, and the buyer’s photos reached our inbox the same afternoon. That notice closed the issue in two emails.
The clause should include segmented deadlines by defect type, a written-notice requirement with photographic evidence, the exact notice content, a defined acceptance test as the trigger for performance objections, a reservation of latent-defect rights, and a statement that silence does not equal acceptance for hidden faults.

The most common mistake I see is a single line: “Complaints must be raised within seven days of delivery.” That line sounds tidy. It is also useless for a cable lug machine. A dented door, a missing die set, and a crimp-force drift are three different problems. They surface at three different times. One deadline cannot cover all of them.
So the first rule in our own contracts is simple. The objection period must be split into segments. Each segment has its own trigger and its own clock.
| Defect category | Clock starts at | Suggested notice window | Evidence required |
|---|---|---|---|
| Transport damage | Unloading | 24–72 hours | Photos of crate and part, carrier note |
| Missing or visibly damaged items | Delivery | 7–14 days | Photos against packing list |
| Apparent technical nonconformity | End of FAT or SAT | 10 business days | Test data, photos, sample lugs |
| Performance failure in production | Discovery by buyer | Reasonable period after discovery | PLC logs, measurements, affected batch |
| Safety-critical defect | Discovery | Immediate, with machine stopped | Photos, alarm history |
Some published machinery terms use 24 hours for damage and a flat 60 days for all testing and detailed defect notice. I treat that as a seller-protective model, not a standard. A 60-day cut-off can quietly erase claims for software faults or tooling wear that only show up later.
In our contracts an objection is only valid if it arrives in writing and carries images. A phone call does not count. A WhatsApp voice note does not count. We ask for a dated email or signed notice, plus photographs or short video of the defect, the die, and the crimped lug. This is not about making life hard for the buyer. It protects both sides. A clear photo of a cracked barrel settles in minutes what a verbal description argues about for weeks. The clause should also list the minimum content: contract number, machine serial number, cable and lug specification, batch number, number of affected units, and the remedy requested.
Performance objections need a measurable anchor. “The machine does not work well” is not an objection. “Crimp height on 95 mm² lugs exceeds the Schedule A tolerance on 6 of 50 samples” is. So the clause should reference the acceptance testing procedures in a schedule. For a Factory Acceptance Test 2 (FAT), I recommend the buyer’s own cable and lug samples and a continuous run of at least four hours before shipment approval. For finished connections, name the standard. IEC 61238-1 governs electrical and mechanical performance 3 of power cable lugs and connectors. DIN 46235 gives dimensional tolerances 4 for tubular lugs. If dies are involved, DIN 48083 Part 4 covers hexagonal die profiles. Naming these turns a subjective complaint into a pass/fail check on non-conforming goods.
Finally, add one sentence that many sellers resist: failure to object within the apparent-defect window does not waive claims for defects that could not reasonably be detected during the agreed tests. I include it in our own templates. It costs us little and removes the buyer’s biggest fear.
A procurement manager in Mexico once asked me why we push spare parts before anything else. My answer: a part on a plane beats a lawyer on a call.
Define a staged claim procedure: an evidence pack, seller acknowledgement within two business days, remote diagnosis, replacement parts for repair or exchange as the first remedy, on-site service if parts fail, retesting against the original acceptance criteria, and a total liability cap equal to the machine price.

A claim procedure should read like a flowchart, not a threat. Here is the sequence I recommend, and it is close to what we use for machines shipped to Canada, India, and the United States.
Why do we put parts first? A cable lug machine is a mechanical and pneumatic system. Most field failures involve a cylinder seal, a sensor, a die, or a control board. Shipping that item by express courier fixes the machine in days. Flying an engineer takes longer and costs more for everyone. The contract should still allow on-site service, but as step five, not step one.
| Evidence item | Why it matters |
|---|---|
| PLC or HMI parameter and alarm logs | Shows force, stroke, and cycle history at the time of failure |
| High-resolution photos or video of defect | Confirms the fault without a site visit |
| Pull-test data from a calibrated tensiometer | Proves the crimp is non-conforming, not just ugly |
| Cable, lug, and die identification | Checks whether the use was inside the approved range |
| Count of affected units and production impact | Sets the defect class and urgency |
Critical means a safety risk or unusable machine. Major means lost production capacity or a repeated quality failure. Minor means cosmetic. I add one guard here. A recurring crimp defect is never “minor” just because the machine still cycles. If the crimp fails IEC 61238-1 values, that is major, full stop.
Here is where buyers push back, and they should ask. Many want production-loss compensation or liquidated damages for downtime. Our position is firm but fair: the maximum total compensation under the contract shall not exceed the contract price 5 of the machine. Without that cap, a ten-person engineering team cannot price the risk of a customer’s entire line stopping. What do buyers get in return? Fast parts shipping at our cost for valid claims, warranty extension for the downtime period, a fresh warranty on replaced parts, and an RCA report. In my experience, that trade is accepted once it is explained. Liquidated damages for late delivery are a separate topic, and I keep them in a separate clause with their own cap.
Every quotation we price forces a choice: a short objection window keeps our risk low, but a window that ignores commissioning reality costs us trust in the next order.
Negotiate 24–72 hours for transport damage, 7–14 days after delivery for visible or patent defects, 10 business days after each acceptance test for performance nonconformities, and 12–24 months of warranty for latent defects, with warranty starting at site acceptance rather than shipment for custom equipment.

Time frames are a commercial negotiation, not an industry law. The table below shows where sellers start, where buyers start, and where I think a fair deal lands.
| Term | Seller-favorable | Buyer-favorable | Balanced compromise |
|---|---|---|---|
| Transport damage notice | 24 hours | 7 days | 48–72 hours with photos |
| Patent defect notice | 7 days from shipment | 30 days from delivery | 7–14 days from delivery |
| Performance objection | Within fixed days of delivery | Any time in warranty | 10 business days after FAT or SAT |
| Latent defects | Excluded after acceptance | Open-ended | Within warranty, clock runs from discovery |
| Warranty period | 12 months from shipment | 24 months from final acceptance | 12–24 months from site acceptance |
| Final payment | 100% before shipment | After 3 months of production | 10–20% released after SAT |
A 12-month warranty period that starts at shipment can lose three months to sea freight, customs, and installation. The buyer may begin production with nine months left. For custom automation equipment 6, I argue the warranty should start at Site Acceptance Test (SAT) or final acceptance. Published machinery terms from large groups like ABB use 12 months as a baseline and cut it to six months for multi-shift operation. I understand the logic. A machine running three shifts wears three times faster. If your plant runs multi-shift, say so in the contract and negotiate the period openly rather than discovering the cut later.
Equipment commissioning is where a custom cable lug machine proves itself. Our installation team connects the buyer’s power supply and compressed air, loads the production dies, and runs the buyer’s actual lugs. Only then can anyone judge cycle time, reject rate, and repeatability. So the performance objection window should open at the end of commissioning, not at the port of arrival. I recommend 10 business days after each acceptance test for apparent nonconformities found in that test.
Sellers want payment certainty. Buyers want performance proof. Both are legitimate. The compromise we use is a milestone structure. A deposit covers materials. A large payment follows the FAT with the buyer’s samples. The final 10–20% is released after a passed SAT under local conditions. If the buyer delays the SAT without cause, the contract should deem acceptance after a fixed grace period. That protects us from a buyer who simply never schedules the test.
One more clock often gets missed. If a crimping cylinder is replaced in month eleven, does it carry one month of cover or a fresh period? I recommend the longer of the remaining warranty or a fixed new period for the replaced part, subject to an overall cap on total warranty duration. Without that, a lengthy repair can leave a new part with only days of coverage.
One lesson from our early export years: a machine that passes a demo with our test lugs can still fail with the buyer’s copper. Specifications must name the buyer’s materials.
Protect your rights by making technical specifications contractual, testing with your own cables and lugs, documenting every deviation in a signed acceptance report, preserving latent-defect claims after final acceptance, requiring retests after repair, and securing staged remedies that end in replacement or price reduction for unresolved major defects.

Promotional words have no legal weight. “High precision” and “stable operation” describe our machines, but they are not acceptance criteria. Technical specifications compliance needs numbers. Our contract annex lists the main machine, crimping head, every die, the approved cable and lug range, the control cabinet and software version, sensors, spare parts, safety guards, manuals, and the utilities required. Each item carries a part number and quantity. Then a separate schedule sets the performance guarantee: crimp height and width tolerance, pull-out force per IEC 61238-1, maximum reject rate over a defined sample, cycle time at a stated configuration, and uptime during the test run. If the machine feeds a downstream line, add integration checks.
A performance guarantee is only as good as the test behind it. So the schedule should state the sample size, the measuring equipment, calibration requirements, and who pays for testing. If we supply the test materials, the contract should say they must match the buyer’s production materials.
Some newer contract ideas are showing up in requests from larger buyers. I do not see them as mandatory, but they are reasonable in the right project.
For aerospace or rail, EN 3373-001 adds qualification, quality assurance, and test programs for crimped terminal lugs that go well beyond normal commissioning. If that is your sector, say so in the contract.
Final acceptance confirms what the tests could see. It cannot confirm what they could not see. Internal hydraulic wear, intermittent sensor faults, and crimp-force drift after thousands of cycles are latent defects. The clause should state that the notice clock for these starts at discovery, that final acceptance does not bar them, and that the claim remains inside the warranty or statutory limitation period under the governing law.
| Seller may fairly exclude | Seller may not hide behind |
|---|---|
| Normal wear of dies and seals | Dies that wear early because of wrong design |
| Use outside the approved cable and lug range | A range stated too narrowly after the fact |
| Utilities outside tolerance | Utility requirements never disclosed in the annex |
| Unauthorized modifications | Settings changed by the seller’s own remote access |
| Lack of scheduled maintenance | Maintenance instructions missing from the manual |
The acceptance report ties all of this together. It should list tests performed, materials used, measured results, deviations, open defects with a responsible party and deadline, retest procedure, and signatures with reservations. We sign it with the buyer’s technical lead at the end of SAT. A signed report with recorded reservations has saved more than one project from an argument about what was agreed on the shop floor.
Vague clauses invite disputes. Segment your objection period, demand written notice with images, put parts first, and cap liability at the machine price. Precise terms protect both sides.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
