
A single under-crimped lug can burn down a switchboard alarm thresholds 1. On our Wenzhou production line, we learned that [in-process checkpoint inspections for cable lug making machines](https://yqunique.com/?p=6056) stop defects early.
To set up in-process checkpoint inspections for cable lug making machines, define measurable pass/fail criteria at five points—material feed, forming, trimming, crimping, and final visual—then inspect first articles after every setup, sample at fixed intervals, record results, and stop the line when critical defects repeat.
That short answer covers the framework. But the details decide whether your system actually catches die wear, crimp drift, and weak joints. Let me walk you through each part, step by step, based on what we do every day in our own workshop.
Last spring, a batch of copper lugs passed final visual checks but failed pull force testing 2 at a customer site. That failure taught our QC team where parameters really matter.
Check barrel geometry, crimp height, palm flatness, hole position, insertion depth, and strand retention at each checkpoint. Add surface checks for cracks, burrs, flash, and plating defects, plus sample pull-out and resistance tests. Tie every parameter to drawing tolerances and classify defects as critical, major, or minor.

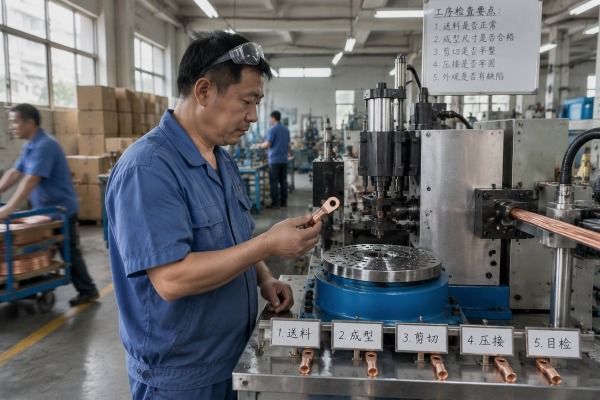
Quality is not one end-of-line test. It is a control system. A cable lug making machine feeds strip stock, forms the lug body, punches the palm and barrel, crimps or compresses, and trims. Each station can create its own defects. So each checkpoint needs its own parameter list.
Here is the checkpoint map we use on our own equipment. It matches the physical flow of the machine, so operators never guess where to look.
| Checkpoint | Key Parameters to Check | Common Defects Caught |
|---|---|---|
| Incoming material | Alloy grade, certificate, thickness, width, hardness, surface | Scratches, pits, oxidation, out-of-spec thickness |
| Setup / first article | Die set match, press parameters, strip length, alignment | Wrong tooling, misalignment, setup errors |
| In-process forming | Palm thickness, hole position, edge condition, die impression | Die wear, burrs, cracked edges, distortion |
| Crimp / compression | Crimp height measurement, die marks, seam, insertion depth | Under-crimping, over-crimping, loose strands |
| Final visual | Plating, flash, bent palms, labeling, traceability | Cosmetic damage, sharp wings, missing marks |
Battery lugs, copper lugs, aluminum lugs, and custom terminals do not share one tolerance set. Aluminum oxidizes quickly, so material integrity verification and surface checks must be tighter. Battery lugs carry high current, so terminal crimping standards for compression uniformity matter more. Our engineers write these differences into the process sheet before the first run.
A cracked barrel is critical. Stop the line. A burr is major. Flag it and check the tooling. Light cosmetic marks are minor. Log them and watch the trend. One more point: write your acceptance limits into the purchase order or quality plan. Never assume them. Dimensional accuracy checks only work when both sides agree on the numbers first.
Every extra checkpoint costs cycle time, and every skipped one risks hidden scrap. We weigh that trade-off on our own line daily before quoting inspection plans to buyers.
Run a mandatory first-article inspection after every setup, tool change, or shift start. Then sample in-process parts every 30–60 minutes or every 500–1,000 pieces, whichever comes first. Re-inspect immediately after alarms, die changes, or material lot changes, and tighten intervals when trends drift.

Some buyers tell me end-of-line inspection is enough. I understand the appeal. It is simple and cheap on paper. But it misses drift, wear, and setup errors that create hidden scrap during the run. By the time the last part fails, hundreds of bad lugs may already sit in the bin. Layered checkpoint inspection with SPC-style trending catches die wear and press variation early, when a small adjustment still fixes the problem.
| Trigger | Inspection Action | Sample Size |
|---|---|---|
| Shift start or setup change | Full first-article approval against drawing | 3–5 pieces |
| Fixed interval during run | Dimensional and visual checks | 3 pieces per interval |
| Tool or die change | First-article approval, mandatory | 3–5 pieces |
| Material lot change | Material integrity and forming check | 5 pieces |
| Machine alarm or abnormal sound | Immediate spot check | 5 pieces |
| Sample basis per run | Pull force testing and resistance check | Per quality plan |
Another objection I hear: tight inspection slows production too much. Our experience says the opposite. Well-designed quality control protocols reduce rework, warranty claims, and unplanned downtime. The key is escalation. If one sample drifts, tighten the interval. If a critical defect repeats, stop the line and run root-cause analysis. If ten intervals pass clean, you can loosen slightly. ISO 9001 compliance also expects documented inspection frequency and records, so this schedule doubles as audit evidence. If your line includes an annealing stage, monitor its temperature and duration in real time on every run, because hardness directly controls crimpability.
A procurement manager from Ohio once asked me for a full gauge list before signing his order. His question shaped the standard inspection kit we now ship with machines.
You need calibrated micrometers and calipers, a crimp height comparator, pin gauges, a pull force tester, and a micro-ohmmeter for resistance checks. Add magnification for visual checks, and consider laser sensors, automated optical inspection, or thermal imaging for high-volume lines. Calibrate everything before each shift.

The right tools turn a checkpoint from an opinion into a measurement. On our line, every gauge has a home position, a calibration record 3, and an owner. Production line calibration happens before the shift starts, not after a bad reading appears. That single habit prevents most measurement disputes.
| Tool | What It Checks | When to Use It |
|---|---|---|
| Digital micrometer / calipers | Strip thickness, palm width, barrel dimensions | Incoming material and forming checkpoints |
| Crimp height comparator | Crimp height against spec | Every crimp checkpoint sample |
| Pin gauges | Hole position and barrel internal diameter | First article and interval checks |
| Pull force tester | Mechanical retention and strand slippage | Sample basis per quality plan |
| Micro-ohmmeter | Contact resistance, electrical conductivity testing | Sample basis, battery and power lugs |
| 10x magnifier or microscope | Cracks, burrs, die marks, plating defects | Every visual checkpoint |
Once volume grows, manual gauges become the bottleneck. Laser sensors can verify barrel internal diameter and palm width automatically during the stamping phase. Automated optical inspection systems confirm marking presence and legibility, including wire size, stud hole diameter, and manufacturer stamps. Ultrasonic sensors can check internal barrel density for hidden voids or inclusions. High-speed thermal imaging spots localized die overheating, which often precedes tool failure. We fit these options during OEM builds when a customer's product mix justifies the cost. But even with full automation, keep the manual kit. A comparator reading settles arguments that a sensor log cannot.
When we build machines for export, we photograph and video every key node—assembly, system debugging, drawing confirmation—for our buyers. That habit pushed us toward PLC-linked digital quality tracking.
Yes. Modern cable lug making machines with smart PLC control can log press force, cycle counts, and sensor readings in real time. Connect inspection stations to the PLC through digital inputs or fieldbus, set alarm thresholds, and export data for SPC trending and full lot traceability.

Remote verification changed how our overseas customers buy. They no longer accept a promise; they expect photo evidence, video confirmation, and logged test data at every milestone. We apply the same logic inside the machine. Here is the integration path we follow when configuring in-process checkpoint inspections for cable lug making machines with PLC tracking.
One caution. More automation does not mean less inspection. Tooling wear and material variation still require physical verification. The PLC tells you when to look; the gauge tells you what is true.
Checkpoint inspections are the cheapest insurance against defective cable lugs. Build them into the machine sequence, measure what matters, record everything, and defects stop before reaching customers.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
1. Wikipedia entry explaining the systems and processes used to manage industrial alarm limits. ↩︎
2. UL provides safety standards and testing protocols for wire connectors and terminals. ↩︎
3. NIST is the federal agency responsible for maintaining national standards for measurement and calibration. ↩︎
4. Official site of the International Organization for Standardization, covering global quality and traceability standards. ↩︎
