
A failed cable lug making machine sample can freeze your whole project. I’ve seen buyers panic here — yet at our Wenzhou plant, we treat it as negotiation, not disaster.
When cable lug making machine samples fail tests, document the failure, verify your drawing parameters first, demand a root cause analysis, and negotiate written corrective action with retest rights. Tie remaining payments to a successful acceptance test, and only approve production after stable, repeatable results.
A failed sample is not the end of the deal. It is the moment you convert test evidence into commercial leverage. Below, I break down exactly how to do that, step by step.
Last year, a procurement manager in Mexico emailed us a single photo and the word "rejected." Our engineers needed far more than that before we could even start fixing anything.
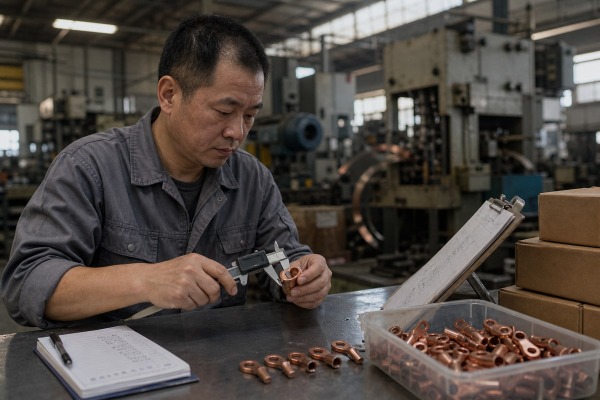
Ask your supplier to explain which test failed, against which agreed specification, and why. Request a written non-conformance report, a formal root cause analysis, machine parameter records, and confirmation of whether your drawing dimensions were followed exactly during sample production.

Vague complaints get vague answers. Structured questions get structured fixes. That is the first rule I teach every buyer who works with our team on terminal manufacturing equipment. Before you talk money, you need clarity on facts.
Send your supplier a detailed technical failure report. Include high-resolution photos, video of the malfunction, and specific measurements compared against the agreed CAD drawings. Then invoke the quality standards 1 and tolerance levels written in your Proforma Invoice or Technical Agreement. This turns your complaint into a formal breach of technical specifications compliance, not an opinion.
| Question to Ask | Why It Matters |
|---|---|
| Which exact parameter failed, and by how much? | Separates critical defects from minor deviations |
| Was the sample made from my final drawing revision? | Catches drawing version errors early |
| What machine settings were used during the sample run? | Reveals calibration or setup mistakes |
| Is the cause mechanical, electrical, or software-based? | Forces a real root cause analysis, not a guess |
| Can you reproduce the failure on your side? | Confirms the problem is real and repeatable |
Demand a written non-conformance report plus a corrective action plan before any retest. In my experience exporting machines to markets like the United States and South Korea, suppliers who resist writing things down usually cannot fix things either. A supplier who answers these five questions with data, not reassurance, is worth continuing with. A supplier who deflects to "operator error" without evidence is showing you a warning sign. Document every answer. You will need this record when negotiation turns to compensation.
Years ago, we chased a crimp height issue for two weeks, then found the customer's drawing listed the wrong barrel wall thickness. That lesson reshaped our entire sample review process.
First, verify your own drawing parameters are correct, because faulty drawings produce faulty samples. Then run repeatability checks: if dimensions drift across cycles, blame machine adjustment or stability. Consistent, wrong-by-design output points to design flaws; random variation points to poor manufacturing or calibration.

From our own sample rejections over the years, failures split into two clear categories. First, the customer's drawing contains an error, so the machine faithfully produces a non-conforming lug. Second, the machine's parameters are badly adjusted or the machine itself lacks stability, so output varies from cycle to cycle. Each case demands a completely different negotiation path, so diagnose before you argue.
| Symptom You Observe | Most Likely Cause | Who Owns the Fix |
|---|---|---|
| Every lug is identical but out of spec | Drawing error or design flaw | Buyer verifies drawing first |
| Dimensions drift over 500+ cycles | Machine stability problem | Supplier must re-adjust and prove stability |
| Random cracks in the crimp barrel | Material hardness mismatch with press settings | Shared — audit material and pressure together |
| Lug fails tensile strength testing at consistent load | Tooling or die design issue | Supplier reworks tooling |
| Failures appear only after long continuous runs | Thermal or hydraulic instability | Supplier corrects and re-demonstrates |
Audit the raw material hardness (HV/HB) of the copper or aluminum lugs used during the test. If the machine's hydraulic pressure settings 2 were tuned for a different copper grade, the crimp will fail even on a healthy machine. Ask for material certification 3 on the test stock. Our engineers always cross-check manufacturing tolerances against the certified material grade before touching any machine setting.
If the drawing checks out and the material checks out, the burden shifts fully to the supplier. Then your demand is specific: re-adjust the machine, prove stable output across repeated runs, and submit to a fresh acceptance test. Do not accept a single "good" piece as proof. Stability, not one lucky lug, is what you are buying.
Every rework negotiation involves a trade-off we know well from both sides: push too hard and the supplier cuts corners; push too soft and you fund their mistakes.
Negotiate supplier-paid rework, replacement samples, and shipping; a written corrective action plan with deadlines; staged payments held until a passing acceptance test; spare tooling such as extra crimping dies as compensation; and a weekly delay penalty. Never release final payment before verified retest results.

Money talks louder than complaints. When our own customers hold back a milestone payment, our engineering team moves faster — I say that honestly, because it is how industrial procurement really works. Your job is to structure that pressure fairly, so the supplier stays motivated rather than defensive.
Present options instead of ultimatums. Here is the sequence I recommend to buyers negotiating with any cable lug making machine supplier, including us:
A supplier confident in their corrective action will accept most of these terms. Hesitation on all six tells you the deeper truth about their capability.
Our sales team once ran a two-hour unedited live stream of a terminal machine producing lugs nonstop, just so a Canadian buyer could approve a retest without flying over.
Protect your next order with written pass/fail criteria before testing, a three-strike clause allowing termination and deposit refund, a virtual factory acceptance test streamed live, retained payment until final acceptance, and a supplier performance evaluation that governs whether future orders continue.

Repeat failures change the question. You are no longer asking "can this be fixed?" You are asking "should this relationship continue?" Modern sourcing practice has shifted decisively toward evidence-based approval: buyers now expect qualification samples from production tooling, measured pass/fail rules agreed in advance, and defined retest rights before any volume order. Build these protections into your contract before the next test, not after the next failure.
| Protection Clause | What It Does | When It Triggers |
|---|---|---|
| Pre-agreed acceptance criteria | Defines pass/fail before testing starts | Every sample and retest |
| Three-strike policy | Terminates the contract with full deposit refund | Third consecutive failure |
| Virtual Factory Acceptance Test (vFAT) | Requires a continuous, unedited live stream of a full production cycle | Before any re-shipment |
| Payment retention | Holds a percentage until final on-site acceptance | Released only after passing |
| Certification requirements | Confirms compliance evidence up front | Before contract signing |
Write your quality control standards directly into the purchase agreement. If your lugs must meet UL certification requirements 4 or specific electrical performance under load, say so explicitly — a supplier cannot honor standards they never saw. Require test videos, measurement reports, and material certification with every sample shipment. Then keep a running supplier performance evaluation: response time, corrective action quality, retest results. When we compete for repeat orders from customers in India, Vietnam, or the US, we know that scorecard decides whether we get the next project. It should decide the same for your suppliers.
A failed sample tests your negotiation skill, not just the machine. Verify drawings, demand evidence, tie money to performance, and put everything in writing before the next test.
1. ISO is the global authority for quality standards and technical specifications in manufacturing. ↩︎
2. Hydraulic pressure settings are critical parameters in the operation of cable lug crimping machinery. ↩︎
3. The IEC provides international standards for the materials and performance of electrical components. ↩︎
4. UL provides the industry-standard safety certification requirements for electrical connectors and lugs. ↩︎
