
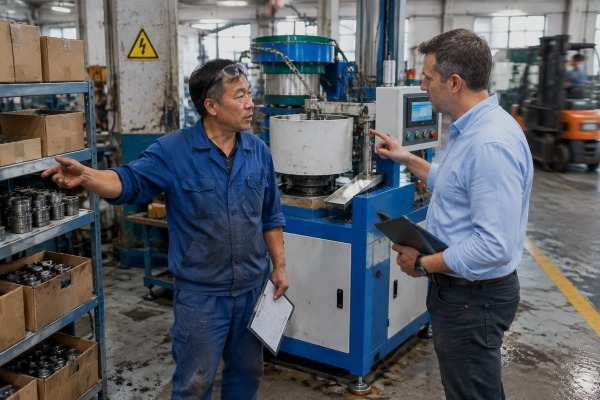
A cheap cable lug machine can turn expensive. On our Wenzhou line, I’ve seen buyers ignore long-term mold and spare parts support for cable lug machines until a die failed.
Evaluate long-term mold and spare parts support for cable lug machines by demanding a serial-number-specific parts list, written availability guarantees of up to ten years, documented die life and wear limits, defined lead times, and a service level agreement covering response and on-site repair.
That sounds like a lot to ask. It is not. The four questions below walk through each piece in the order a buyer should raise them UL 486A-486B 1. I will also share the one habit that saves our customers the most downtime: writing the long-term spare parts list before the contract, not after the first breakdown.
Every time we quote crimping die sets, I weigh two numbers: the unit price today and the replacement price in year five. Buyers usually ask only about the first.
Before signing, ask for expected die life by application, wear limits, sharpening intervals tied to stroke counts, replacement price with a price-review mechanism, manufacturing lead time, modular insert options, refurbishment services, and whether dies are revision-controlled and reproducible from a serial number.

First, a note on words. On our forming and crimping machines, "mold" can mean the crimping die, the compression die, the forming tool, or a dedicated fixture on the press. Each one wears at a different rate. So the first thing I ask a buyer is which tooling they actually mean.
I do not accept that claim from my own toolroom, and you should not accept it from any supplier. Tool life depends on conductor size, lug material, crimp force, contamination, alignment, lubrication, speed, and setup quality. Copper and aluminum lugs wear a die differently. A worn or flattened die will keep running. It will just produce a slowly changing crimp geometry that still looks fine to the eye. That is the real danger.
So I ask suppliers to show a maintenance ledger. It should tie die sharpening intervals to specific stroke counts and record what happened after each repair. If the ledger does not exist, the life claim is a guess.
| Question to ask | Why it matters | What a strong answer looks like |
|---|---|---|
| What is the expected life for my exact lug and cable range? | Life by application, not a generic number | A tooling matrix with cross-section, lug material, crimp profile, and stroke-count estimate |
| What are the wear limits and inspection intervals? | Lets you replace before scrap appears | Written limits with measurable dimensions and a tooling maintenance schedule |
| Is the die modular? | Lets you replace a high-wear insert, not the whole assembly | Insert drawings and insert prices listed separately |
| Can the die be refurbished? | Regrinding and recoating extend life | A formal refurbishment program with turnaround time |
| Are dies serialized and revision-controlled? | Replacement must match the original | Reproduction from serial number plus revision notices |
| What is the replacement price and lead time in year three? | Prevents price shock later | A price-review mechanism and a stated manufacturing lead time |
Here is the point I push hardest. Do not judge a supplier by whether it has spares in stock today. Confirm that it can still supply the matching dies, wear parts, and key components for the next several years. The practical tool is a long-term spare parts list, written during negotiation. It lists each die set, each wear part, the price, and the lead time. Never let your first price request for a die happen after the machine stops.
I also ask buyers to keep a tooling health record: machine serial, die-set ID, installation date, crimp count, materials processed, inspection results, pull-test results, and replacement date. That record separates die wear from machine faults. It also makes precision die manufacturing on our side easier, because we know exactly which revision we are reproducing. For emergencies, negotiate native 3D CAD files or controlled drawings so a local toolmaker can cut a replacement.
A procurement manager in the United States once asked me to prove our wear parts inventory with photos, not promises. That request changed how we present stock to every buyer.
Verify spare parts inventory by requesting a serial-number-linked parts list with original manufacturer part numbers, current stock status, standard and maximum lead times, and emergency shipping options. Then test it: order one sample consumable and time the delivery before the contract is signed.

A generic catalog is not a spare parts list. The list you want is tied to the bill of materials of your machine's serial number. Each line should name the part, its function, the original manufacturer, the part number, approved alternatives, lead time, and criticality. When a supplier cannot name the original manufacturer of a sensor or valve, that is a warning sign.
| Category | Examples on a cable lug machine | What to confirm |
|---|---|---|
| Fast-moving consumables | Dies, blades, seals, filters, clamps, fasteners, bowl feeder wear strips | Stock on hand, minimum order quantity, shelf life, price |
| Repairable service parts | Pneumatic cylinders, valves, motors, sensors, power supplies | Repair or exchange option, warranty, approved substitutes |
| Long-lead or obsolete-risk parts | PLC, servo drive, HMI, proprietary boards, custom tooling | Obsolescence status, last-time-buy process, retrofit path |
The rule we follow is simple. Map every spare to the equipment bill of materials. Then set a stocking policy by criticality and lead time. High-criticality, long-lead items get safety stock. Low-risk items can rely on the supplier's commitment.
Buyers often ask for a fixed ten-year parts availability commitment. Suppliers of our size will push back, and the reason is fair: third-party electronics can go obsolete without warning. My answer is to not drop the demand but to reshape it. Accept a shorter guaranteed period if the supplier provides open documentation, named alternatives, a documented retrofit path, and the freedom to source standard components yourself.
One more trap. Do not compare spare part unit prices alone. A low-cost sensor with a twelve-week lead time can cost more in lost production than a higher-priced local equivalent available in a day. For critical parts, qualify a second source. But run every substitution through change control, because an unapproved die or sensor can change crimp quality and void warranty.
The hardest lesson from shipping cable lug machines to Germany and Japan was simple. Those buyers read the warranty exclusions before they read the specification sheet.
Expect a written warranty that covers crimping dies and control components, a service level agreement with separate acknowledgment and diagnosis targets, remote diagnostics, calibration and pull-test procedures, serial-number-specific documentation with PLC backups, and operator training verified by practical tests.

A warranty is only as good as its exclusions. Read them first. If the excluded items are exactly the parts most likely to fail, such as dies, seals, and sensors, the warranty is decorative. I tell buyers to ask for the warranty duration and the exclusion list side by side.
Evaluate after-sales technical support as its own organization. Sales people are friendly before the order. The service team is who you call at two in the morning. Ask about support hours and time zones, language capability, escalation steps, and whether emergency support exists outside business hours. Ask about the first-time fix rate for emergency breakdown requests. A supplier that tracks this number is a supplier that manages its service.
| Metric | What to define | Why one number is not enough |
|---|---|---|
| Acknowledgment time | Hours until a ticket is confirmed | A four-hour acknowledgment can still hide a multi-day diagnosis |
| Diagnosis time | Hours until root cause is identified | This is the number that controls downtime |
| Remote resolution target | Share of tickets closed without travel | Many PLC and parameter issues can be solved remotely |
| On-site response | Days until an engineer arrives | Depends on regional coverage, not on promises |
| Parts dispatch | Hours from approval to shipment | Links service to the spare parts list |
Remote diagnostics on a smart PLC machine cut downtime. But the contract must state who owns the machine data, how access is authorized, and what cybersecurity controls apply. Ask what happens if a cloud service is discontinued. If IoT sensors monitor hydraulic pressure and vibration, ask how that data feeds predictive maintenance rather than just alarms.
A machine can run perfectly and still make bad crimps. So support must include process verification. Ask which standards the machine and tooling support, by name. Depending on your market and end use, these may include IEC 60352-2 3 for solderless crimped connections, UL 486A-486B for wire connectors in North America, DIN 46235 4 for compression cable lug dimensions, and IPC/WHMA-A-620 5 for harness workmanship. A supplier should name the applicable ones, not use vague compliance language.
Request the factory acceptance test, the site acceptance test, calibration certificates, the crimp-force verification method, pull-test requirements, and the recalibration interval. Make calibration documentation a purchasing requirement.
Insist on user and maintenance manuals, exploded drawings, electrical and pneumatic schematics, the parts list, PLC and HMI backups, parameter backups, alarm-code explanations, a tooling maintenance schedule, and a revision history. All of it must be specific to your serial number. Training should end with a test, not a demonstration. Operators should prove they can change a die, recover from a common alarm, verify a crimp, and complete the maintenance checklist. Ask for a train-the-trainer package with fault simulations.
When our engineers retrofitted a newer PLC onto an older forming machine, the customer's first question was not about the controller. It was whether his existing dies would still fit.
Assess long-term reliability by checking the supplier's installed base, the age of its oldest supported machine, its policy for parts on machines older than ten years, documented obsolescence notices with last-time-buy options, retrofit examples that preserve existing tooling, and customer references in comparable applications.

That retrofit question is the whole topic in one sentence. Control electronics go obsolete before the frame and the press. Vendor reliability assessment is therefore about whether the supplier plans for that, not whether it exists today.
Ask how long the supplier has built this machine family, not how long the company has existed. Then ask: How many machines of this model are still in service? What is the oldest supported installation? Which components have already gone obsolete? How were legacy machines upgraded? What percentage of service requests are solved remotely? Ask for references with similar lug materials, conductor sizes, and production volumes. A supplier that handles low-volume manual presses well may struggle with a high-throughput automatic line.
If the supplier cannot identify installed machines, parts histories, or completed upgrades, treat that as a red flag.
A documented modernization roadmap beats a promise to "support the machine as long as possible." Ask for the current control-system generation 6, the expected support horizon, the migration path, whether old parameter files carry over, estimated retrofit cost, the downtime needed for conversion, and whether the upgrade preserves existing tooling. Ask for an obsolescence notification period and a last-time-buy process in writing.
| Evaluation area | Suggested weight |
|---|---|
| Tooling range and compatibility | 15% |
| Tooling quality, validation, and expected life | 15% |
| Spare parts availability and lead times | 15% |
| Service response and regional coverage | 15% |
| Documentation and training | 10% |
| Calibration and quality support | 10% |
| Obsolescence and upgrade plan | 10% |
| Total cost of ownership | 5% |
| Supplier financial stability and references | 5% |
Shift the weights to your situation. A high-volume automotive or utility plant should weight uptime and validation higher than purchase price.
Buyers often tell me a local service company is more reliable than an overseas builder. There is truth in that for travel time. But a local shop rarely has design authority over the die geometry or the PLC program. The hybrid model works best: OEM engineering support plus trained local maintenance capability. That is how we structure support for distributors in the United States and Europe, and it is why we certify local technicians rather than fly for every fault.
Finally, run the total cost of ownership over ten to fifteen years: purchase price plus tooling, maintenance, spares, service, downtime, and retrofits, minus residual value. Then compare any premium for a longer availability guarantee against the cost of one prolonged stoppage. Long-term mold and spare parts support for cable lug machines is a production-risk decision, and this calculation makes that visible.
A low machine price hides years of tooling, repairs, and downtime. Build your long-term spare parts list before signing, and buy the support system, not just the machine.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
1. Authoritative body for safety standards regarding wire connectors in North America. ↩︎
2. International standard-setting body relevant to manufacturing quality and precision processes. ↩︎
3. Official source for the international standard governing solderless crimped connections. ↩︎
4. German national organization for standardization covering compression cable lug dimensions. ↩︎
5. Global trade association for the electronics industry and harness workmanship standards. ↩︎
6. Leading professional association for the advancement of technology and electronic systems. ↩︎
