

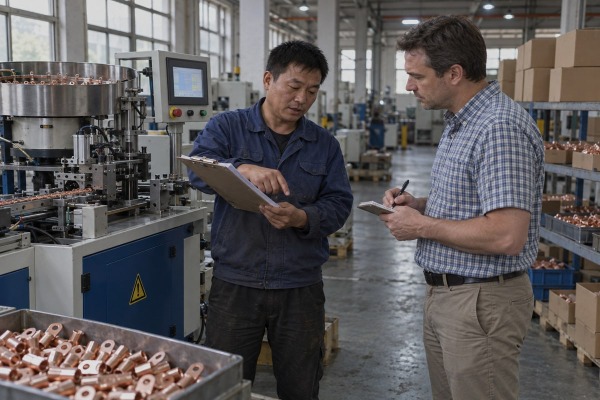
Buyers emailing our Wenzhou workshop often focus on price alone. Weak support means downtime later. Assessing a supplier’s professionalism and support when buying a cable lug machine prevents that pain.
Assess a supplier’s professionalism and support when buying a cable lug machine by checking six things: product knowledge, understanding of your cable and lug requirements, technical response speed, documented sample testing, after-sales capability including spare parts and warranty, and communication efficiency. Demand written evidence, not brochure claims.
Those six checks sound simple. In practice, each one needs specific questions and specific documents. The four sections below walk through them in the order a real purchase usually follows.
A procurement manager from the US once sent us only a cable cross-section 1 and asked for a quote. We sent back eleven questions first. That exchange changed his shortlist.
Look for a supplier that asks technical questions before recommending a model. It should request conductor material, cross-section range, strand class, lug barrel dimensions, crimp profile, production volume, and applicable standards, then explain in writing why a specific hydraulic, servo, or pneumatic configuration fits your application.

Cable cross-section alone tells us very little. Outside diameter, strand class, insulation thickness, and terminal geometry all change the tooling. So before our engineers recommend a forming or crimping configuration, we work through a fixed list of inputs. A supplier who skips this list is guessing, and you will pay for the guess later.
| Input the supplier should request | Why it matters to the machine specification |
|---|---|
| Conductor material: copper, aluminum, or both | Changes die profile and compression ratio |
| Cross-section and outside diameter range | Sets the tooling range and machine force |
| Solid, stranded, flexible, or sector-shaped conductor | Affects fill ratio and crimp geometry |
| Lug and connector material, barrel dimensions, wall thickness | Determines die cavity size and required force |
| Crimp profile: hexagonal, circumferential, diamond, or indent | Selects the die family |
| Number and position of crimps | Defines positioning fixtures |
| Target volume and cycle time | Decides manual, semi-automatic, or wire processing automation with a bowl feeder |
| Pull-out force 2, resistance, and visual limits | Becomes your acceptance criteria |
| Power supply, floor space, environment | Drives installation requirements |
| Applicable standards such as IEC 61238-1 3, UL, DIN | Confirms tooling and lug compatibility |
We judge a salesperson, including our own team, on six points: product knowledge, understanding of the requirement, technical response, willingness to run sample tests, after-sales capability, and communication efficiency. A simple test covers all six. Send real samples or complete technical data. Ask for a written recommendation. Then compare the reply. Does it address the complete process, or does it just repeat the advertised capacity? A machine advertised for terminals up to roughly 400 mm² can still fail on one specific terminal geometry. Professional tooling portfolios may cover about 6–630 mm², but that range is a starting point, not proof. An honest supplier names the limits of each model instead of claiming one machine handles everything.
Buyers in Germany often ask whether to go direct. Going direct gives you access to the application engineers who can run wire-terminal compatibility analysis and custom die design. An authorized distributor may offer faster local service, local stock, and easier warranty handling. The practical answer is to ask for both: direct engineering contact plus a named local service partner. Also ask where the machine is actually built and who owns the company. If the sales company is only an intermediary but presents itself as the factory, that is a red flag.
Our hardest lesson came from a shipment to Mexico that sat in customs for weeks. The warranty clock had already started at shipment. We changed our contract wording after that.
Evaluate after-sales service and warranty policies by reading the actual contract terms: warranty start date, covered components, wear-part treatment, response time, parts and labor coverage, and spare parts availability after expiry. Then verify named technical contacts, remote diagnostic capability, and local service options in writing.

Equipment warranty terms should be read as a service commitment, not a marketing line. Most disputes we have seen come from wording that was never defined. The table below shows the gap between vague wording and wording that protects a buyer.
| Contract item | Weak wording | What to request instead |
|---|---|---|
| Warranty start | From the date of shipment | From installation and commissioning sign-off |
| Wear parts | "Consumables excluded" | Dies, seals, blades, and sensors listed with expected cycle counts |
| Response time | "Full support provided" | Named contact, maximum response hours, escalation path |
| Labor and travel | Not mentioned | Stated coverage for engineer visits |
| Repeated failure | Not mentioned | Replacement remedy after a defined number of failures |
| Parts after expiry | Not mentioned | Availability period for controllers and electronics |
One more distinction matters. A warranty repairs a failed hydraulic pump. A performance guarantee states that the machine will achieve specified crimp dimensions, force, cycle time, and defect levels. Ask for both.
A factory can be technically strong and still give poor service if every repair depends on a distant headquarters. So ask who the named technical contacts are and which time zones they cover. Our team supports customers from the US to Japan, so we schedule response windows rather than promising "24/7" without staff behind it. Ask about remote diagnostics through the PLC. Ask whether the supplier can give real-time, over-the-shoulder guidance by video call or AR platform for troubleshooting. Then raise the obvious objection: remote support cannot replace hands. That is true for hydraulic leaks, mechanical alignment, and die seating. The resolution is to ask which fault types remote support covers and who attends on site for the rest, with a stated arrival time and locally stocked dies, hydraulic parts, and electrical components.
Ask whether installation is done by the manufacturer, an authorized technician, or your own staff, and whether travel is included. Commissioning should include production trials on approved cable and lug combinations. Operator training programs should cover both operation and maintenance, with materials in your language. Finally, insist on a signed commissioning record listing the serial number, software and firmware versions, tooling installed, approved recipes, test results, outstanding defects, training completion, acceptance date, and warranty start date. That one document prevents most later arguments about what was delivered.
Two batches of nominally identical copper strip reached our lug forming line last spring. One ran harder. Our sample measurements caught the dimension drift before shipment.
Ask which standards cover the machine, the tooling, and the finished crimp separately. Request ISO 9001 certification scope, factory acceptance testing procedures, calibration certificates, and sample reports showing crimp dimensions, pull-out force, and electrical resistance on your actual cable and lugs across multiple repeated samples.

That copper strip story is why we never trust a single photograph of a finished crimp. Material varies in hardness, wall thickness, plating, and tolerance even when the part number is the same. Quality control has to be verified as a process, in this order.
| Report field | What it should show |
|---|---|
| Machine model, serial, tooling and die code | Traceability of the exact setup |
| Lug and conductor specification | Match to your production material |
| Crimp dimensions and force or pressure | Comparison against acceptance limits |
| Cycle time and number of crimps | Realistic throughput |
| Pull-out or tensile result | Mechanical performance |
| Resistance or voltage drop, where applicable | Electrical performance |
| Visual defects: cracks, burrs, distortion, incomplete compression | Hidden defect check |
| Results across repeated samples | Repeatability, not a single good part |
Certificates deserve scrutiny. ISO 9001 certification 4 indicates a quality management system. Check the issuing body, the scope, the validity date, and whether it covers manufacturing or only trading. It does not prove a crimp. Terminal crimping quality standards such as IEC 61238-1, UL requirements, IEC 60228, and DIN specifications apply to lugs, conductors, and the completed crimp, not to the machine frame. For the machine itself, ask for a declaration of conformity, CE documentation where applicable, a risk assessment, and calibration certificates. Ask whether machine calibration services are offered after delivery and at what interval. Then address the common objection head-on: a certificate says the product conforms to a standard, but only application-specific sample testing proves your combination works. Finally, for a PLC-controlled line, ask what the touchscreen system logs. Some systems record crimp force, die code, date, time, and tool serial number per crimp. That level of traceability matters for automotive, energy, and railway customers.
Proprietary dies or universal clamping—we weigh this on every OEM project in our Wenzhou shop. Tighter control versus buyer freedom. Neither answer is free.
Determine long-term support capability by checking custom die set manufacturing, a priced two-year spare parts list, PLC firmware lifecycle and cybersecurity policy, tooling interoperability, and references from customers running the same model for three years. Score suppliers on total cost of ownership, not purchase price.

A machine can idle for weeks because a low-cost sensor, seal, or controller is no longer available, even when the frame and hydraulics are perfectly sound. Long-term support is therefore part of machine selection, not something to sort out after purchase.
Ask for a recommended two-year spare parts list with prices, part numbers, minimum stock quantities, and lead times. Ask about local inventory and emergency order procedures. Then ask whether standard industrial components are used. We build around standard PLC, pneumatic, and sensor components so a buyer in Italy or India is not locked to a single source for every part. Here the trade-off is real: proprietary parts can improve integration, while generic parts are easier to source but complicate support if substitutions are not approved. Ask for an approved substitution list. Also ask about PLC firmware 5 lifecycle and the cybersecurity policy for networked machines, since the control system will outlive several network standards. Finally, request power consumption per 1,000 cycles so you can compare running cost across suppliers.
Your lug range will change. A supplier should document die profile and dimensions, compatible lug families, die material and hardness, expected die life, the die-change procedure, the coding system, and whether dies can be adapted for future lug designs. Ask directly whether the quoted price includes all required dies or only a basic set. Back to the opening trade-off: proprietary tooling supports traceability and consistent quality, while universal die-clamping standards allow third-party tooling and avoid vendor lock-in. Our resolution on OEM/ODM projects is to state the clamping standard in the quotation so the buyer chooses with full information.
| Criterion | Suggested weight |
|---|---|
| Technical fit | 25% |
| Sample-test performance | 20% |
| Support and response capability | 15% |
| Documentation and training | 10% |
| Warranty and contractual protection | 10% |
| Spare parts availability | 10% |
| References and financial stability | 5% |
| Purchase price and total cost of ownership | 5% |
Adjust the weights to your risk. A continuous production line should push service and spare parts even higher.
Ask for references running the same model for at least three years with similar cable sizes and volumes. Ask them about on-time delivery, achieved cycle time, reproducibility of sample results, fault response speed, parts availability, unexpected costs, and whether they would buy again. Red flags include refusal to give references, inconsistent company names, copied product images, unverifiable certificates, generic manuals with mismatched model numbers, pressure to pay quickly, and unclear bank-account ownership.
Price comparisons feel safe but hide downtime risk. We tell every buyer: choose the supplier that proves technical fit, documents acceptance tests, and commits to lifetime parts and support.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
1. Provides technical context for electrical conductor sizing and cross-sectional area measurements. ↩︎
2. Explains the mechanical testing principles used to verify the strength of a crimped connection. ↩︎
3. The International Electrotechnical Commission is the governing body for the cited crimping quality standard. ↩︎
4. Official source for the quality management standard used to evaluate supplier manufacturing processes. ↩︎
5. Authoritative reference for cybersecurity and lifecycle management of industrial control systems. ↩︎
