
Your cable lug making machine lands at the dock with no engineer attached. Our Wenzhou team has watched idle machines cost more than freight. Planned remote startup guidance prevents that.
Arrange remote startup guidance for a cable lug making machine by writing it into the purchase contract: define installation, power-on, commissioning, and training steps, name responsible contacts on both sides, set session counts and response times, and agree what triggers an on-site visit.
That one sentence hides a lot of work. Below, I break it into four practical questions. Each one covers what the guidance includes, how to prepare, what tools you need, and how to confirm your team is ready.
A procurement manager in Texas once asked me over WhatsApp whether remote support meant a phone number. For our copper lug production lines, it means a documented sequence.
Remote startup guidance includes pre-sale application review, sample validation, a live factory acceptance test, a site-readiness review, video-guided installation and power-on, parameter loading, trial production, online operator training, maintenance training, and a signed acceptance record with ongoing technical support.

The phrase cable lug making machine covers very different equipment. Remote guidance that works for one type can fail for another. So I separate them before I quote.
| Machine type | What it does | Remote startup fit |
|---|---|---|
| Terminal crimping machine (compact press) | Crimps finished lugs onto cable, often listed for 6–120 mm² | High; video calls usually cover it |
| Hydraulic terminal press, around 200 kN | High-force hexagonal or indent crimps on power-cable lugs | Medium; needs electrical and tooling checks |
| Cold pressing terminal machine or lug forming press | Forms, punches, and bends copper or aluminium lugs | Medium to low; die alignment is critical |
| Automatic copper lug production line with bowl feeder | Sorts, feeds, forms, and inspects lugs continuously | Low for remote-only; hybrid is safer |
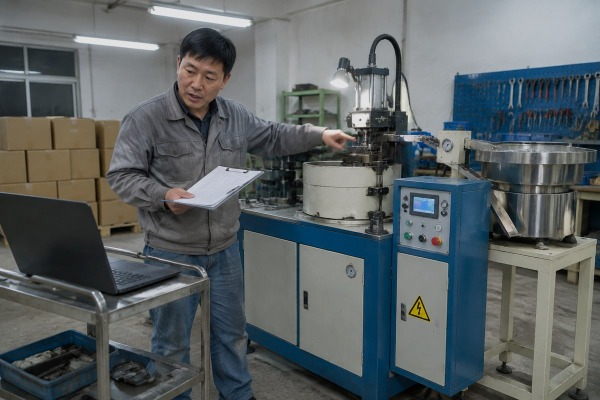
Our automatic forming machine with the vibratory bowl feeder 1 sits in the last row. The PLC timing, the feeder, and the die seat all interact. That is why we do not promise a remote-only startup for it until a sample test is done.
If our engineer cannot travel, I put the whole remote path into the contract. Each step has an owner and a deadline.
The contract should separate equipment defects, buyer installation errors, unsuitable materials, operator error, and later application changes. It should also state the condition that converts remote support into an on-site visit, and who pays travel. Without that line, both sides argue about the same idle machine.
One lesson from shipping to Mexico stuck with me: a wrong phase configuration found on power-up day wasted a whole scheduled session. Preparation starts weeks earlier.
Prepare by completing a site-readiness checklist, confirming voltage, frequency, phase, earthing, and compressed air, clearing floor space and access routes, assigning named electrical and mechanical staff, stocking approved cable and lug samples, and sending the supplier photos and a video walkthrough in advance.

Most delays I see are not about the machine. They are about the room around it. So I ask buyers to confirm these points in writing before we book the first call:
A written checklist can still hide problems. A two-minute phone video of the installation bay shows me blocked panels, poor cable routing, or a workbench placed where the bowl feeder stand needs to go. I review the video, mark up a layout drawing, and send it back before anything is unpacked.
Remote sessions fail when nobody owns a task. So I ask for named people, not departments.
| Role | Responsibility before the session |
|---|---|
| Project owner | Signs the checklist and approves acceptance criteria |
| Electrician | Verifies supply, earthing, motor rotation, and cabinet lockout |
| Mechanical technician | Handles lifting, leveling feet, transport lock removal, and die storage |
| QC inspector | Holds approved samples and prepares the pull tester and resistance meter |
| Operators | Attend every session and keep the logbook |
Approved cable and lug samples, lug drawings, and material certificates must be on site before power-on. The trial run is compared against those samples, not against a catalogue figure. If the buyer's copper alloy batch differs in hardness from the validation batch, we adjust pressure settings during the trial and record the change.
During a virtual commissioning for a German distributor, a single phone camera could not show the die seat and the PLC screen at once. We lost an hour.
You need a stable internet connection, two or more cameras for synchronized views, a dedicated WhatsApp or Zoom channel, a VPN-based PLC remote access module, exploded-view diagrams, a video installation manual, calibrated measuring tools, and crimp testing equipment to verify finished joints during the first run.

| Item | Purpose during remote startup |
|---|---|
| Two cameras on tripods or clamps | One on the tooling area, one on the control panel |
| Headset with microphone | Clear audio next to a running press |
| Dedicated chat channel | WhatsApp or WeChat for quick photos, Zoom for the live session |
| VPN or secure gateway to the PLC | Lets our engineer read fault history and load recipes |
| Exploded-view diagrams and 3D models | Shared reference to bridge language gaps |
| Video installation manual | Step-by-step clips for mold changing, blade replacement, and PLC resets |
| Crimp height gauge and calipers | Geometric check of each trial crimp |
| Pull-out tester and micro-ohmmeter | Mechanical and electrical proof of the joint |
| Thermal camera, optional | Spots friction or heat build-up on first high-speed cycles |
Two views are the minimum. Our engineer needs to see the hand on the die and the screen at the same time. A wired connection or a strong hotspot avoids frozen frames at the moment a transport lock is removed. We also keep photos flowing on WhatsApp during the call, because a still image often shows a misaligned barrel better than video.
A PLC remote access module shortens troubleshooting. It also opens a door. So our technical support protocol is simple: access is temporary, the buyer authorizes each session, parameters are backed up before any change, every change is logged, and the buyer can switch the link off locally. Firmware updates go through the same approval.
Looking at a crimp is not enough. A joint can look clean and still fail. So the first-run checks include crimp height, visual inspection for cracks or cut strands, a pull-out test, and a resistance or voltage-drop reading. Some buyers add AI visual inspection for lug geometry or augmented reality technical support with shared on-screen markers. Those help, but the gauge and the tester are what sign the acceptance sheet. Blockchain commissioning logs are sometimes mentioned online; in practice, a signed PDF log with timestamps is what warranty and insurance reviewers ask for.
We weigh a real trade-off here: one long training call is cheap to schedule, but split modules with sign-off sheets are what actually stick on a night shift.
Ensure understanding by splitting training into operator and maintenance modules, recording every session, issuing quick-reference guides, requiring competency sign-off per task, running a supervised production acceptance test against IEC or UL crimp criteria, and keeping a technical support protocol with named contacts and response times.

I never run one general call. The operator and the maintenance technician need different content. Each module ends with a sign-off sheet that lists the task, the person, the date, and the trainer.
| Module | Operator training | Maintenance training |
|---|---|---|
| Startup and shutdown | Yes | Yes |
| Loading cable and lug, feeder adjustment | Yes | — |
| Recipe selection and basic parameters | Yes | Backup and restore |
| Visual inspection and rejection handling | Yes | — |
| Clearing jams and emergency-stop response | Yes | Yes |
| Daily cleaning and lubrication | Yes | Intervals and wear parts |
| Die inspection, sensor replacement | — | Yes |
| Hydraulic or pneumatic checks | — | Yes |
| Fault-code interpretation and escalation | Basic | Full |
Every session is recorded. The buyer keeps the recording in a local digital library next to the video installation manual, so a new hire two years later can watch the die change for the same machine.
Understanding is proven on the acceptance run, not on a quiz. The buyer's operators run production under our remote supervision. The QC inspector checks the joints against the standard that applies to the destination market:
A machine marked CE does not certify the joint. The certification belongs to the complete system: cable, lug, die, settings, and operator. So the acceptance sheet records all five.
Buyers tell me that remote-only startup shifts the risk onto them. They are partly right. Poor camera angles, language barriers, and a thin local team can hide alignment or vibration faults. My answer is not to pretend remote is always enough. It is to build a hybrid path into the after-sales service agreement: remote review, remote factory acceptance test, remote basic installation, live trial, and a defined on-site trigger if the trial fails acceptance or the line is custom and high volume. The agreement also lists training hours, number of sessions, time zone coverage, supported languages, warranty start date, spare-parts list, and post-warranty support rates. That is how informal help becomes a system your team can rely on.
An unsupported machine sits idle and burns schedule. Write the remote path into the contract, prepare the site, equip the call, and sign off trained people.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
1. Technical explanation of the sorting and feeding mechanism used in automated production lines. ↩︎
2. Official international standard for solderless crimped connections and testing requirements. ↩︎
3. Safety standard for wire connectors and lugs used in North American electrical systems. ↩︎
4. German technical standard specifying dimensions and requirements for compression cable lugs. ↩︎
5. International standard governing the electrical and mechanical performance of power cable lugs. ↩︎
