
Key takeaway: An optical inspection machine can only detect a defect that is visible, presented to the camera, resolved by the optics, separated by lighting, and represented in the decision model. Define the defect library before choosing cameras or speed.
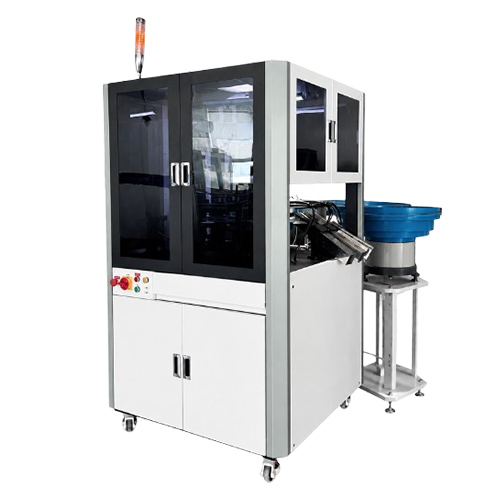
Automatic visual inspection uses cameras, lenses, lighting, part handling, software, and reject mechanisms to classify parts. A glass-turntable or vision-sorting machine can inspect small components from multiple views at production speed, but performance is application-specific. A camera count or megapixel figure does not establish detection capability.
The strongest projects begin with defect samples and clear acceptance rules. Buyers should define part families, surface finishes, dimensions, presentation state, critical defects, minimum defect size, false-accept risk, false-reject tolerance, traceability, and changeover needs.
Terms such as scratch, discoloration, incomplete feature, burr, crack, wrong assembly, or deformation are too broad for machine design. Each defect should be described by location, geometry, contrast, size, orientation, and severity. If people disagree on the boundary between good and bad samples, the vision system will inherit that uncertainty.
Build a labelled sample library containing normal variation, boundary samples, known defects, and deliberately created challenge pieces. Preserve information about material lot, process condition, and human disposition so image results can be traced back to the quality decision.
For engineering support on a similar project, review product design services.
Inspection capability is limited by the weakest link from feeding through rejection.
| Subsystem | Purpose | Key verification |
|---|---|---|
| Feeder and presentation | Separate and orient parts | Jam rate, surface damage, stable pose, recirculation |
| Optics and cameras | Resolve the feature in the field of view | Pixel scale, depth of field, distortion, focus stability |
| Lighting | Create contrast and suppress unwanted reflections | Part color/finish variation, contamination, aging |
| Decision software | Measure or classify features | Threshold control, model version, boundary samples, audit trail |
| Reject and sorting system | Route each inspected part | Timing, air pressure or mechanism, confirmation, fail-safe behavior |
For a related YQUNIQUE product example, review glass turntable optical inspection machine.
A false accept allows a bad part into good output; a false reject sends a conforming part to reject or reinspection. Tightening a threshold often reduces one while increasing the other. Acceptance should therefore report both rates for each defect family and the tested product mix.
Add an uncertainty path rather than forcing every image into good or bad when image quality is inadequate. The machine can reject, stop, or route uncertain parts for review. Camera obstruction, feeder instability, poor orientation, or missing views should be detected as process faults, not silently classified.
The factory acceptance protocol should include sustained throughput, feeder replenishment, changeover, normal stop/restart behavior, known-good parts, known-bad parts, boundary samples, and reject confirmation. Record every challenge sample’s expected and actual destination.
After installation, repeat critical tests under site lighting, vibration, utilities, and operator conditions. Establish routines for lens cleaning, light-intensity verification, reference samples, backups, calibration, software/model control, and review of saved images.
For engineering support on a similar project, review factory automation equipment design.
For engineering support on a similar project, review custom solutions.
Enough spatial resolution for the smallest required feature across the actual field of view, with suitable optics and contrast. Megapixels alone do not determine detectability.
No. Any decision method needs representative labelled evidence and clear acceptance rules. Sample quality and coverage remain central to validation.
No single metric is sufficient. Report false accepts, false rejects, unclassified parts, sustained throughput, and reject-routing accuracy for the defined sample set.
Optical inspection success comes from a visible, measurable defect definition and a controlled chain from part presentation to reject confirmation. Start with samples and decision rules, then select the cameras, lighting, software, and handling architecture.
YQUNIQUE provides glass-turntable optical inspection and custom automation solutions. Share drawings, production samples, defect samples, speed, changeover, and data requirements for a feasibility review.
For application-specific requirements, contact YQUNIQUE.
Technical note: Inspection performance claims are valid only for the defined parts, defect library, presentation, optics, lighting, recipe/model version, test sample, and acceptance method. Revalidate after material, finish, tooling, software, or optical changes.
