
Our Wenzhou line once scrapped a tray of thin-walled shaft sleeves. They left a fully automatic chamfering machine slightly oval. That hurt. The fix was the fixture, not the automation.
Not necessarily. A fully automatic chamfering machine will not deform thin-walled shaft sleeves when the sleeve is supported internally, clamped with evenly distributed force, cut with sharp tooling at light feeds, and cooled properly. Deformation comes from uneven clamping, unsupported walls, dull tools, chatter, and heat, not from automation.
So the real question is not whether the machine is automatic. The real question is how the sleeve is held, how the cutter meets the edge, and how you verify the result. I will walk through each of those below.
The hardest lesson we learned in thin-walled part processing is simple. The sleeve does not care how fast the machine is. It only cares about force and stiffness.
Deformation when chamfering thin-walled shaft sleeves comes from force exceeding the wall's stiffness. The main causes are concentrated clamping pressure, an unsupported bore, high cutting resistance from dull or badly angled tools, chatter from aggressive feeds, heat from poor cooling, and residual stress released from earlier forming.

A sleeve wall resists radial load 1 poorly. Push on one point and the wall moves. If the force stays below the yield point, the sleeve springs back when released. That is elastic deformation. The chamfer was still cut on a distorted shape, so the finished edge is wrong even though the part looks round later. If the force passes the yield point, the wall stays bent. That is permanent workpiece deformation, and no later step fixes it.
| Cause | How it acts on the wall | What we see on the bench |
|---|---|---|
| Concentrated clamping pressure 2 | Three jaws push at three points; hydraulic or pneumatic chucks add more force than the wall needs | Three-lobe roundness error, dents at jaw contact |
| Unsupported bore | The cutter pushes the edge inward with nothing behind it | Collapsed or rolled chamfer edge, inward taper |
| Dull tool or wrong rake angle | The edge rubs instead of cutting, so axial pressure rises | Burrs, heat marks, chamfer size drifts |
| Aggressive feed and chatter | The low-mass wall vibrates with the cutter | Wavy chamfer, cyclic size error, micro-cracks in brittle alloys |
| Heat | The wall expands during the cut and shrinks after | Parts measure fine warm and fail cold |
| Residual stress 3 | Cutting removes material that was holding stress in balance | Part springs out of round even with light clamping |
Lowering clamping pressure sounds like the obvious fix. It is not enough on its own. A sleeve that is held too lightly can slip, rotate off center, or vibrate. Then the chamfer becomes uneven and the part can still be damaged. The goal is enough holding force spread over a wide area, not simply less force.
Cold-drawn, rolled, welded, or heat-treated blanks carry locked-in stress. Chamfering cuts away a ring of material that was helping hold that stress. The part relaxes and changes shape. When I see distortion that does not match the jaw count, I look at the blank before I blame the machine. The same rule applies to metal pipe chamfering.
The ratio of wall thickness to diameter decides how much load the wall can take. I will not give you a single cutoff number. Stiffness also depends on length, material, hardness, and support. My field rule is this: if you can squeeze the sleeve out of round by hand, treat it as a critical part and plan a fixture trial.
Every fixture we design for a sleeve balances two risks. Too much grip ovalizes the wall. Too little lets it slip and chatter. Neither is acceptable.
Choose fixtures that spread load evenly and back the wall from inside. Full-contact collets, bored soft jaws, or expanding mandrels beat standard three-jaw chucks. Add regulated pneumatic or hydraulic pressure, dual-stage clamping, a positive axial stop, and keep the fixture end face close to the chamfering cutter disc.

Workholding is the single biggest lever you have. Here is how the common options compare for thin sleeves.
| Workholding | Radial pressure distribution | Internal support | Best fit | Main risk |
|---|---|---|---|---|
| Standard three-jaw chuck | Three concentrated points | None | Thicker walls, short runs | Three-lobe distortion |
| Bored soft jaws | Wide arc contact | None | Medium walls, repeat jobs | Jaw wear, chips trapped under the jaw |
| Full-contact collet | Even around the circumference | None | Thin walls of moderate length | Over-closing still ovalizes the part |
| Fixed mandrel with light external clamp | Even | Full bore backing | High-volume parts with a consistent bore | Tight loading clearance, chip trap in the bore |
| Expanding mandrel | Even, from inside | Adjustable | Very thin or long sleeves | Over-expansion stretches the bore |
This is the first thing I check on any new sleeve job. I do not start with speeds. I clamp a sample, measure it while held, release it, and measure again. If the roundness error has a pattern that matches the number of jaws or collet slots, the fixture is squeezing unevenly. Soft jaws bored to the exact sleeve diameter spread contact over a wide arc. A full-contact collet spreads it further. For the thinnest walls we put a mandrel inside so the wall is pinched between two surfaces instead of pushed from one side.
This is the second check, and most people skip it. The distance between the fixture end face and the cutter disc is the unsupported overhang. Think of it as a lever arm. The longer that arm, the more the cutter can bend the edge. We set that gap as small as cutter clearance and burr escape allow. On our machines the glass viewing windows let the operator see this gap directly during setup, so it does not drift after a fixture change.
A pneumatic clamping system gives repeatable force, but repeatable is not the same as correct. The pressure must be set and verified on the actual part. Dual-stage clamping logic helps here. The machine uses higher pressure to seat the sleeve against the axial stop, then drops to a lower holding pressure during the cut. Servo-controlled or programmable force takes this further. The fixture body itself also needs structural rigidity. A flexible fixture moves with the cutter, and the sleeve follows it.
A procurement manager in the US once asked me for the right feed rate for his sleeves. I asked for his drawing first. Parameters follow the part.
Reduce stress by cutting light and sharp. Use low feed per revolution, shallow chamfer depth, sharp inserts with positive rake, a stable spindle speed that avoids chatter, short tool overhang, steady coolant flow, and adaptive torque monitoring. Develop values through trials on your actual sleeve, not from generic charts.

I will not print a feed-and-speed table for every material. That would be dishonest. Diameter, wall thickness, hardness, cutter type, and chamfer size change the answer. What I can give you is the direction each parameter should move for thin walls, and why.
| Parameter | Direction for thin walls | Reason |
|---|---|---|
| Spindle feed rate (per revolution) | Low | Cutting force rises with chip load |
| Chamfer depth per pass | Shallow, use two passes if needed | Less radial engagement at any moment |
| Spindle speed | Moderate, tuned to avoid chatter | Too fast builds heat; the wrong speed excites vibration |
| Rake and clearance angles | Positive and sharp | Lower cutting resistance and less axial pressure on the edge |
| Tool overhang | As short as possible | Rigidity on the tool side keeps the cut stable |
| Entry and exit | Smooth ramp, no plunge | Avoids a shock load on the thinnest part of the edge |
| Part support length | Maximum | Shortens the unsupported lever arm |
This is my third standing check, after fixture force and cutter distance. Heat is quiet. A sleeve expands during the cut, gets chamfered at the larger size, and shrinks after. On aluminum and copper alloys this shows up fast. I confirm that the coolant reservoirs are full, the filter tray is clean, and the nozzle is aimed at the cutter contact, not at the fixture. Our units carry twin liquid reservoirs for exactly this reason. We also let parts reach room temperature before gauging. Measuring a warm sleeve tells you nothing useful.
Spindle-load or torque monitoring turns the machine into a sensor. When a tool starts to rub, the load rises before the burr is visible. Adaptive feed control can slow the spindle feed rate when resistance spikes, which protects soft non-ferrous walls from crushing. Ultrasonic-assisted chamfering modules are advertised to cut required force by up to half. That is a supplier claim, so we treat it as something to verify in a trial, not as a given.
A worn edge changes every number in the table above. We replace tooling when burr height, spindle load, or chamfer width starts to drift, not when the insert looks bad. Sharp tooling is the cheapest form of precision deburring.
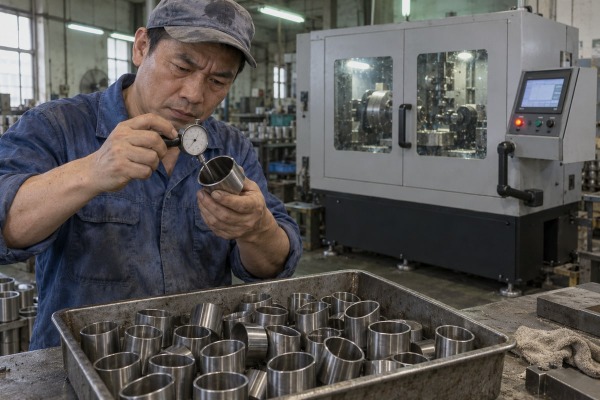
During a sample test for a Mexican client, our QC bench found sleeves that passed diameter checks but failed roundness. That gap changed how we inspect.
Confirm sleeves are deformation-free by measuring roundness, wall thickness, inside and outside diameter, concentricity, chamfer size, and burr height before machining, while clamped, and after release. Compare parts from the start, middle, and end of a run, then repeat with a worn tool to find the process limit.

Inspection has to match the function of the part. A sleeve that fits a bearing cares about roundness and concentricity 4. A diameter check alone can pass a three-lobed part. Here is the validation sequence we run before we sign off a machine for a customer.
| Characteristic | Method | Note |
|---|---|---|
| Roundness | Roundness tester or air gauge | Diameter alone misses lobing |
| Inside and outside diameter | Air gauge, bore gauge, micrometer | Measure at room temperature |
| Wall thickness | Micrometer at several points around the ring | Uneven blanks distort on their own |
| Concentricity | Coordinate-measuring machine | Required for bearing and hydraulic fits |
| Chamfer angle and width | Optical projector or vision system | Also detects missing chamfers |
| Burr height | Vision system or profilometer | Burr growth signals tool wear |
| Surface finish | Roughness tester | Chatter marks show up here first |
Buyers tell me that automation repeats a bad setup at high speed. That is true. A fully automatic chamfering machine with a poor fixture produces a full bin of oval sleeves before anyone notices. The answer is not to avoid automation. The answer is in-process gauging, automatic rejection of out-of-tolerance parts, and a validated fixture before volume starts. Done this way, the automated cell gives better dimensional accuracy than a manual bench because the clamping force, tool path, and cycle time stop changing from operator to operator.
Ask what minimum wall thickness they have processed, how clamping force is set and verified, whether internal support is standard, and whether they will run your sample parts and send back measured roundness data. A capability claim without sample parts is just a sentence.
Thin-walled shaft sleeves do not fear automation. They fear force without support. Fix the fixture, cutter distance, and cooling, verify with measurement, and a fully automatic chamfering machine stays safe.
Interested in sourcing the products mentioned in this article? See details and request a quote here:
1. Explains the mechanical response of thin-walled structures to external forces. ↩︎
2. NIST research discussing the impact of clamping forces and workholding on machining precision. ↩︎
3. Authoritative NIST publication on how internal stresses affect part distortion during machining. ↩︎
4. Official ISO standard for geometrical tolerancing, including concentricity and form. ↩︎
5. Overview of surface texture characteristics and measurement in manufacturing. ↩︎
