

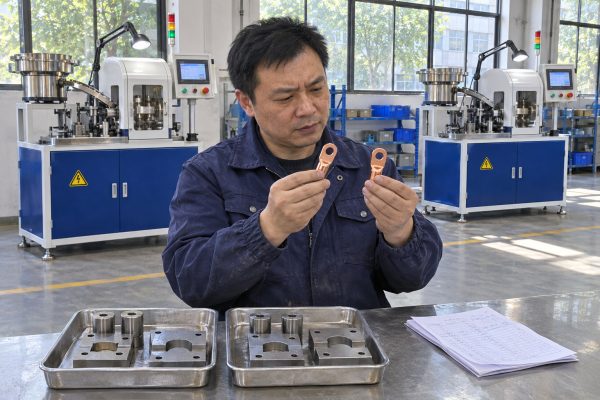
One hydraulic valve delay once idled a customer’s entire terminal line for weeks. From our Wenzhou workshop, I urge buyers to qualify backup suppliers for cable lug making machines early.
To diversify supply risk with backup suppliers for cable lug making machines, qualify at least two verified vendors at first purchase, confirm they share no factory or critical components, test samples with your own cable, duplicate dies and software backups, and contract response times and reserved capacity.
That sounds like a lot of work. It is less work than restarting a stopped line. Below, I walk through how we help buyers find, qualify, and maintain a second source step by step.
A procurement manager in the US asked our team last year whether two quotes from different brand names meant two factories. Often, they do not.
Identify reliable backup suppliers for cable lug making machines by starting with a vendor risk assessment of your own line, then shortlisting manufacturers from different regions, verifying the real factory behind each quote, checking shared sub-suppliers, and screening technical fit against one common specification.

The biggest mistake I see is searching for a second machine before understanding the first one. A backup supplier only matters if it covers a gap you actually have. So the search starts inside your own plant, not on a sourcing platform.
Before I send a single inquiry, I ask buyers to classify each cable lug machine and process. The list is short but revealing:
This assessment tells you what kind of backup you need. A shop producing a narrow range of standard lugs may only need a validated second machine and duplicate tooling and die sets. A high-volume plant feeding utility or data-center projects may need geographically separated lines and pre-negotiated emergency capacity.
Market listings describe industrial crimping-machine demand as growing roughly 5–7% per year, driven by grid modernization, renewable energy, and electrification. Treat that as an indicative estimate, not a verified statistic. But the direction is clear, and capacity is tight in peak seasons. Asia-Pacific remains the main production hub, which brings cost advantages and concentration risk. Two suppliers in the same industrial cluster can share the same port congestion, power rationing, or regulatory shock.
That is why many buyers now use a "supplier + 1" approach. Deloitte cites a Gartner survey in which 57% of industrial manufacturers operating in China were considering adding a second source outside one company or country. A sound multi-sourcing strategy measures separation at the factory, component, tooling, and shipping-route levels.
| What looks like diversification | What real diversification requires |
|---|---|
| Two brand names, one factory behind both | Verified factory addresses and manufacturing scope |
| Two assemblers, same hydraulic valve and PLC brand | Bill-of-materials review for critical industrial automation components |
| Two suppliers, same city and same port | Different regions, corridors, and currency exposure |
| Two quotes, two different specifications | One common technical specification sent to both |
When we quote a line from Wenzhou, we are open about which components we build and which we source. Ask every candidate the same question. Supply chain resilience depends on the honesty of that answer.
During a factory acceptance test on one of our terminal forming lines, the machine cycled perfectly, yet the first aluminum samples looked wrong under the inspection lamp. Motion is not quality.
Qualify a secondary equipment supplier on technical capability first: cable cross-section range, copper and aluminum compatibility, crimping force, die availability, PLC control systems, and repeatability. Then verify the factory, run sample trials under IEC 61238-1 or UL 486A-486B, and retain 10–20% payment until site acceptance.

I treat qualification as a staged process. Each stage filters out a different kind of weak supplier. Skipping a stage usually saves two weeks and costs six months later.
| Standard | Scope | When I reference it |
|---|---|---|
| IEC 61238-1 | Compression and mechanical connectors for power cables | Finished crimp performance on power-cable lugs |
| DIN 46235 | Compression cable lugs for copper conductors | Lug geometry and dimensional acceptance |
| DIN 48083-4 | Coded dies for compression tools | Die coding when standardizing tooling across suppliers |
| UL 486A-486B | Wire connectors for copper and aluminum conductors | North American customer requirements |
These standards are not interchangeable. The buyer should state which standard governs the product, the machine, the tooling, and the finished crimp. We write that into the inquiry and the purchase contract, and we expect any secondary supplier to accept the same wording.
Beyond standards, I score every candidate on cable cross-section range, conductor class and strand construction, lug wall thickness, crimping force or pressure, cycle time, changeover time, automatic or manual loading, machine footprint and utility requirements, safety features, and documentation. A vibratory feeder bowl and a touchscreen look impressive in photos. The repeatability data decides.
Every time we quote a non-standard line, I weigh open-architecture PLC controls against a cheaper proprietary board. The cheaper board usually costs more the day you switch suppliers.
Maintain consistent quality across multiple suppliers by issuing one common technical specification, standardizing die coding and measurement methods, testing finished lugs rather than machine motion, securing PLC programs and parameter backups, duplicating critical tooling and die sets, and requalifying samples annually with the same acceptance protocol.

Switching suppliers mid-production is where most quality drift happens. The machine changes, the dies change, the operator habits change, and the measurement method quietly changes too. Consistency comes from controlling what stays the same.
The specification is the anchor. It defines cable sizes, lug materials, die references, allowable dimensional variation, sample counts, operators, and test methods. Both suppliers build to it. Both suppliers get tested against it. If one of them later proposes a design change, the change goes through the same document.
In practice, I push buyers to standardize three things even when full interchangeability is impossible:
Some of the most useful resilience tools are engineering decisions made before purchase. Open-architecture PLC control systems allow a second integrator to read, back up, and modify the program without a proprietary lock. Modular die-insert designs let an independent precision machine shop cut replacement tooling without waiting for the original builder. A digital blueprint escrow for critical mechanical parts gives you drawings for local or additive production if the primary chain fails. Predictive maintenance telemetry 3, shared with the backup supplier, tells them when wear parts are approaching replacement so they can stage inventory before you call.
| Item to secure | Why it matters during a switch |
|---|---|
| Electrical drawings and PLC programs | A second technician can diagnose and restore the line |
| Parameter and recipe settings | Reproduces proven crimp results on the backup machine |
| Die drawings and maintenance schedules | Independent shops can remake worn tooling |
| Raw material traceability records | Separates material lot problems from machine or die problems |
| Manuals and troubleshooting procedures | Operators keep the same work instructions on both machines |
When we deliver a line, we hand over program backups and parameter sheets as standard. If a buyer's primary supplier does not, the contract should fix that before the backup is ever needed. Quality is only consistent when the knowledge is portable.
The lesson I took from shipping lines to eight export markets is simple: a dormant backup quietly expires. Prices age, tooling drifts, and capacity vanishes.
Build a risk-resilient supply chain by mapping every single point of failure, choosing a redundancy model such as 80/20 dual sourcing or capacity reservation, contracting response times and reserved slots, stocking risk-based spare parts, comparing expected disruption loss with backup cost, and running quarterly reviews and emergency drills.

Dual sourcing and backup sourcing are not the same thing. Dual sourcing means actively buying from two approved suppliers. A backup supplier may receive little or no routine volume but stays contractually and technically ready. Dual sourcing gives stronger readiness at higher cost. A dormant backup is cheap but often fails when activated. Your production line redundancy model should sit somewhere on that spectrum, based on how much downtime you can afford.
| Model | How it works | Best fit |
|---|---|---|
| Primary-plus-backup (100/0) | Main supplier gets all routine orders; backup only does test work | Low disruption probability, strong spare-part stock |
| 80/20 or 70/30 split | Secondary gets enough business to stay familiar and interested | Most practical compromise for mid-to-high-volume plants |
| Equal split (50/50) | Both suppliers carry similar volume | Maximum redundancy, lower volume discounts |
| Regional split | One supplier per plant or market | Multi-site operations with strong standardization |
| Capacity reservation | Retainer or minimum volume buys emergency production slots | When a complete second machine is too expensive |
I hear this often, and it is partly right. Multiple suppliers mean more audits, more tooling inventory, more training, lower discounts, and more complex maintenance support. A single strategic supplier can offer deeper engineering collaboration and lower total cost for stable, low-risk products.
But the visible savings from single sourcing can be erased by one extended outage. So I ask buyers to run one simple framework:
Expected annual disruption loss = probability of disruption × financial impact of disruption
Include lost sales, expedited freight, idle labor, contractual penalties, customer loss, and recovery costs in the impact figure. Compare the result with the annual cost of a qualified backup. The number carries uncertainty. It is a decision tool, not a forecast. In my experience, once a buyer prices idle labor and penalties honestly, the 80/20 model usually wins.
The backup agreement must state whether the supplier is merely approved or holds reserved capacity. Write in activation response time, maximum quotation and delivery times, price-adjustment rules, spare-parts availability period, remote support, software backups, warranty, acceptance tests, force-majeure boundaries, and subcontractor disclosure. Do not rely on penalties alone. A supplier can accept a penalty clause and still be unable to ship during a regional crisis. Reserved capacity and periodic test orders are worth more.
Pair the backup with risk-based inventory: critical dies for the highest-volume lug sizes, hydraulic seals and pumps 4, sensors, relays and power supplies, PLC and drive components, fuses, contactors, and calibration equipment. This supports lead time optimization without stocking an entire second machine.
Then govern it. Run quarterly supplier risk reviews, annual sample requalification, periodic emergency-order drills, and capacity confirmation before peak seasons as part of your manufacturing capacity planning. Track on-time delivery, defect rates, response time, and spare-parts fill rate on one dashboard, alongside price.
A single supplier failure can stop a healthy plant. Qualify two verified sources at first purchase, separate them geographically, test real products, and keep the backup active.
1. Authoritative technical documentation for the PLC control systems used in industrial cable lug machinery. ↩︎
2. ISO 9001 is the primary global standard for the quality certifications required during supplier qualification. ↩︎
3. Wikipedia provides a comprehensive overview of predictive maintenance technologies used to monitor industrial equipment health. ↩︎
4. Updated manufacturer product page for industrial hydraulic components and pumps. ↩︎
