

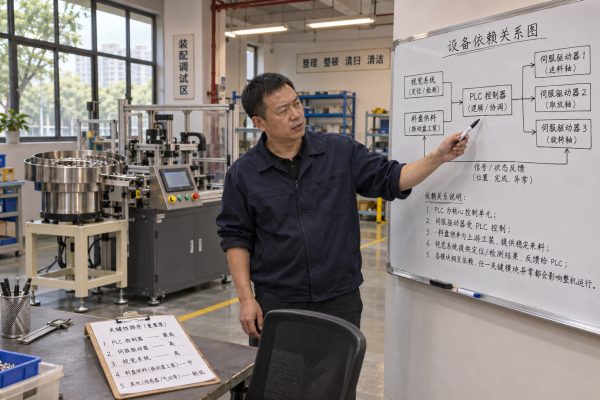
Backup suppliers for automatic assembly machines rarely get budget until a line stops. One late servo drive shipment to our Wenzhou shop taught me that lesson painfully.
Build backup suppliers for automatic assembly machines by mapping every machine dependency, ranking equipment by criticality, qualifying a tiered group of alternates through samples and small orders, standardizing interfaces and documentation, giving backups a small share of live work, and re-evaluating every supplier on a fixed schedule.
That is the short version. The long version is what follows. I will walk through how we find alternates, how we score them, how we keep production running during a switch, and how we keep several suppliers engaged for years. I will also be honest about the costs, because a second supplier is not free.
A US procurement manager once asked me for a list of our competitors. He wanted a second source for a terminal crimping cell, and I respected that.
Identify reliable backup suppliers for automatic assembly machines by searching several channels at once, building a tiered long list instead of one alternate, checking for shared sub-tier dependencies, and prequalifying each candidate against references, capacity, and service coverage before any quotation.

He was doing the right thing. A single machine builder is a hidden single point of failure. Even if the machine is sitting on your floor, you may still depend on that one builder for the PLC program, the vision system license, the custom feeder tooling, and the technician who knows the alarm codes. So the search for a backup has to cover more than "who else can build this cell."
My first rule is simple. Keep a tier of suppliers, not one replacement. When we source servo drives 1, pneumatic cylinders, and bowl feeder components for our own assembly machines, we keep a primary, a qualified backup, and one or two prequalified candidates. If the backup also has a problem, we are not starting from zero. The same logic applies when you buy complete machines. One alternate is better than none, but a tier is what gives you real supply chain resilience.
Our second rule is to look in several places at the same time. Each channel shows you a different kind of supplier.
| Channel | What it tends to reveal | Weakness |
|---|---|---|
| Trade exhibitions | Machine builders with demo cells you can touch | Only shows who paid for a booth |
| B2B platforms such as Made-in-China | Wide long list, fast quotation response | Capability claims need checking |
| Component makers (PLC, robot, vision brands) | Integrators certified on that platform | Pushes you toward their ecosystem |
| Customer and industry references | Suppliers who already survived a real ramp-up | Small sample size |
| Regional engineering networks and integrators | Local service capacity, module-level alternates | May not build complete machines |
A multi-sourcing strategy that uses only one channel usually finds the same three well-known names everyone else finds.
Two suppliers in different cities may buy the same servo motor, the same camera, and the same PLC from the same factory. That is not diversification. Part of the supplier risk assessment should be a short questionnaire on sub-tier sources, country of origin, and export exposure. We answer these questions for our own customers, and I expect our sub-suppliers to answer them for us.
It also helps to remember that a backup does not have to be a second complete machine builder. Three types of backup exist: a second builder, a second source for critical modules and tooling, and a service alternative such as an independent integrator or a trained in-house maintenance team. Rank each dependency with a simple score: operational impact times disruption likelihood times recovery difficulty. A low-cost sensor with a long lead time can score higher than the machine frame itself.
The cheapest vibratory bowl feeder 2 vendor we ever qualified failed its first small-batch order on surface finish. That lesson now shapes every scorecard we use.
Evaluate a backup supplier with one unified scorecard covering technical capability, quality validation, delivery capacity, service and spare parts, financial strength, geographic resilience, controls compatibility, cybersecurity, and total cost, then confirm the score with sample tests and a small batch order.

The lesson from that feeder vendor was not "avoid cheap suppliers." The lesson was that we had no common standard. One engineer judged on price, another on delivery, and nobody wrote down what "acceptable" meant. So we built a single vendor qualification process 3 and we apply it to every candidate, whether they supply a bracket or a complete chamfering machine.
Here is the structure I recommend. The weights come from a research framework we found practical, and we adjust them by machine criticality.
| Criterion | Weight | What we actually check |
|---|---|---|
| Technical capability | 20% | Comparable cycle time, accuracy, changeover, safety design |
| Quality and process validation | 15% | Inspection records, change control, acceptance test history |
| Delivery capacity and lead time | 15% | Backlog, engineering headcount, ability to build several machines at once |
| Service and spare parts support | 15% | Response time, technician coverage in your region, parts stock |
| Financial and business continuity | 10% | Ownership stability, years in operation, continuity plan |
| Supply chain and geographic resilience | 10% | Sub-tier sources, tariff and export exposure, logistics routes |
| Controls, software, data compatibility | 5% | PLC and HMI platform, protocols, recipe formats |
| Cybersecurity 4 and remote access | 5% | Secure remote maintenance, credential handling, update policy |
| Total cost of ownership | 5% | Purchase price plus parts, service, and energy over five years |
For a regulated process, I would push validation and documentation higher and price lower. For a simple sorting station on a blue steel frame, cost can carry more weight.
Three words matter here. An approved supplier has passed commercial checks. A qualified supplier has passed technical validation. A production-ready supplier can deliver, install, support, and ramp inside your recovery window. Most companies stop at "approved" and believe they have a backup. They do not.
Paper scores are a start, but we verify real ability in stages:
Step four is where that feeder vendor failed. It was a small order, so the failure cost us little. That is the whole point of staging the vendor qualification process. Ask about surge capacity too. A supplier who can build one prototype may not be able to build four production machines in the same quarter.
Last year we rebuilt the PLC program for a customer's assembly cell because the original builder had left no backup file. The machine was fine. The knowledge was gone.
Maintain continuity by backing up drawings, PLC programs, licenses, and tooling data before any switch, holding a critical spare parts inventory of long-lead items, standardizing interfaces so modules interchange, and rehearsing the transition with a tabletop exercise and a real quotation from the backup.

That rebuild took weeks of downtime that a single USB backup would have prevented. Switching suppliers is not a purchasing event. It is an engineering event, a maintenance event, and an IT event. The work has to be done before the switch, not during it.
Every machine we ship leaves with a documentation package, and I tell customers to demand the same from every builder. The list should include:
Alongside documents, keep a critical spare parts inventory. Focus on long-lead items with high recovery difficulty: servo drives, controllers, cameras, proprietary cylinders, and worn feeder tooling. These items give you time. Lead time mitigation does not come from the backup supplier alone; it comes from the buffer that lets the backup supplier finish their work.
Full machine interchangeability is expensive. Most of our customers do not need it. They need the right level.
| Level of interchangeability | What it means | When it pays off |
|---|---|---|
| Complete machine | Backup builds an equivalent cell | Bottleneck lines, sole production sites |
| Module or station | Feeder, press, or inspection station swaps in | Modular machines with defined interfaces |
| Tooling | Equivalent fixtures and change parts from a second shop | High-wear or product-specific tooling |
| Controls and drives | Same PLC family, drive family, protocols | Mixed fleets with one maintenance team |
| Spare parts | Common catalog components across builders | Every plant |
| Service personnel | Cross-trained technicians or local integrator | Remote plants with slow vendor response |
Component standardization at the interface level is usually the best return. Specify open protocols, standard HMI alarm structures, and widely supported PLC and drive brands. Then let each builder keep some design freedom. Interchangeability of parts at the module level gives most of the benefit at a fraction of the cost.
Contingency planning that has never been tested is an assumption. We run simple drills: ask the backup to quote and schedule a defined replacement, time how long it takes to retrieve the program files, and request real lead times for the top ten spare parts. Include IT in the drill. Remote support, cloud dashboards, and connected HMIs widen the attack surface, so access control, network segmentation, and secure remote maintenance belong in the same continuity plan.
Giving a backup supplier 10% of our orders costs us some volume discount from the primary. I accept that cost, because an idle backup forgets how to build our parts.
Build long-term relationships by allocating orders gradually so backups stay engaged, choosing a sourcing model that fits each machine's criticality, writing contracts with spare parts and transition support clauses, auditing performance regularly, and re-evaluating every supplier on a fixed annual cycle.
The trade-off is real, and it is the first objection I hear from procurement managers. "Why pay more per unit for a supplier I may never need?" My answer is that the question is framed wrong. The right question is "What does it cost to stay single-sourced?" Add up downtime per hour, expedited freight, emergency tooling, contract penalties, and the customer you lose because a launch slipped. Against that number, a modest premium for a warm backup is small.
A backup that gets no work for three years loses the engineers who learned your process. It may also change its control platform without telling you. So we feed backups a steady trickle. Small recurring orders, spare part production, or a maintenance contract all work. The models look like this:
Choose the model per machine, not per company. A bottleneck crimping line and a bench-top sorting unit do not deserve the same treatment.
Contracts cannot prevent disruption. They can keep your options open. The clauses I consider essential are maximum response and repair times, guaranteed availability of critical spare parts, obsolescence notification periods, engineering change approval, notification of major sub-tier changes, rights to recover tooling and documentation, and exit assistance during a transition. For buyers worried about intellectual property 5 with two suppliers, I suggest sharing performance specifications rather than the incumbent's drawings. That protects both the buyer and the builder.
Our seventh rule is a fixed re-evaluation cycle. Once a year we rescore every active supplier against the same scorecard used at qualification. Delivery performance, quality escapes, service response, and any ownership or location changes all feed in. A supplier can move up a tier or down a tier. This is not punishment. It is how the tier stays honest.
One industry summary reports that fewer than 29% of supply chains are considered future-ready, and only 6% reach leading maturity across mapping, continuity, supplier assurance, and digital integration. Definitions vary between studies, so treat those figures as a signal rather than a benchmark. The signal is clear enough: most companies say resilience matters and few have tested it.
Single sourcing feels cheap until the line stops. Then every hour costs more than the backup would have. Map dependencies, qualify a tier, keep data portable, and test the switch early.
1. IEEE is the leading authority for technical standards in electrical and electronic engineering components. ↩︎
2. Provides a technical definition and mechanical overview of the specific automation component mentioned. ↩︎
3. The International Trade Centre (ITC) provides resources on international procurement and supplier qualification standards. ↩︎
4. NIST provides the primary cybersecurity framework for protecting industrial control systems and manufacturing data. ↩︎
5. WIPO is the global forum for intellectual property services, policy, and information. ↩︎
